Home › Field notes › Custom Modular Bag Cost Breakdown: Every Line That Moves Pricing
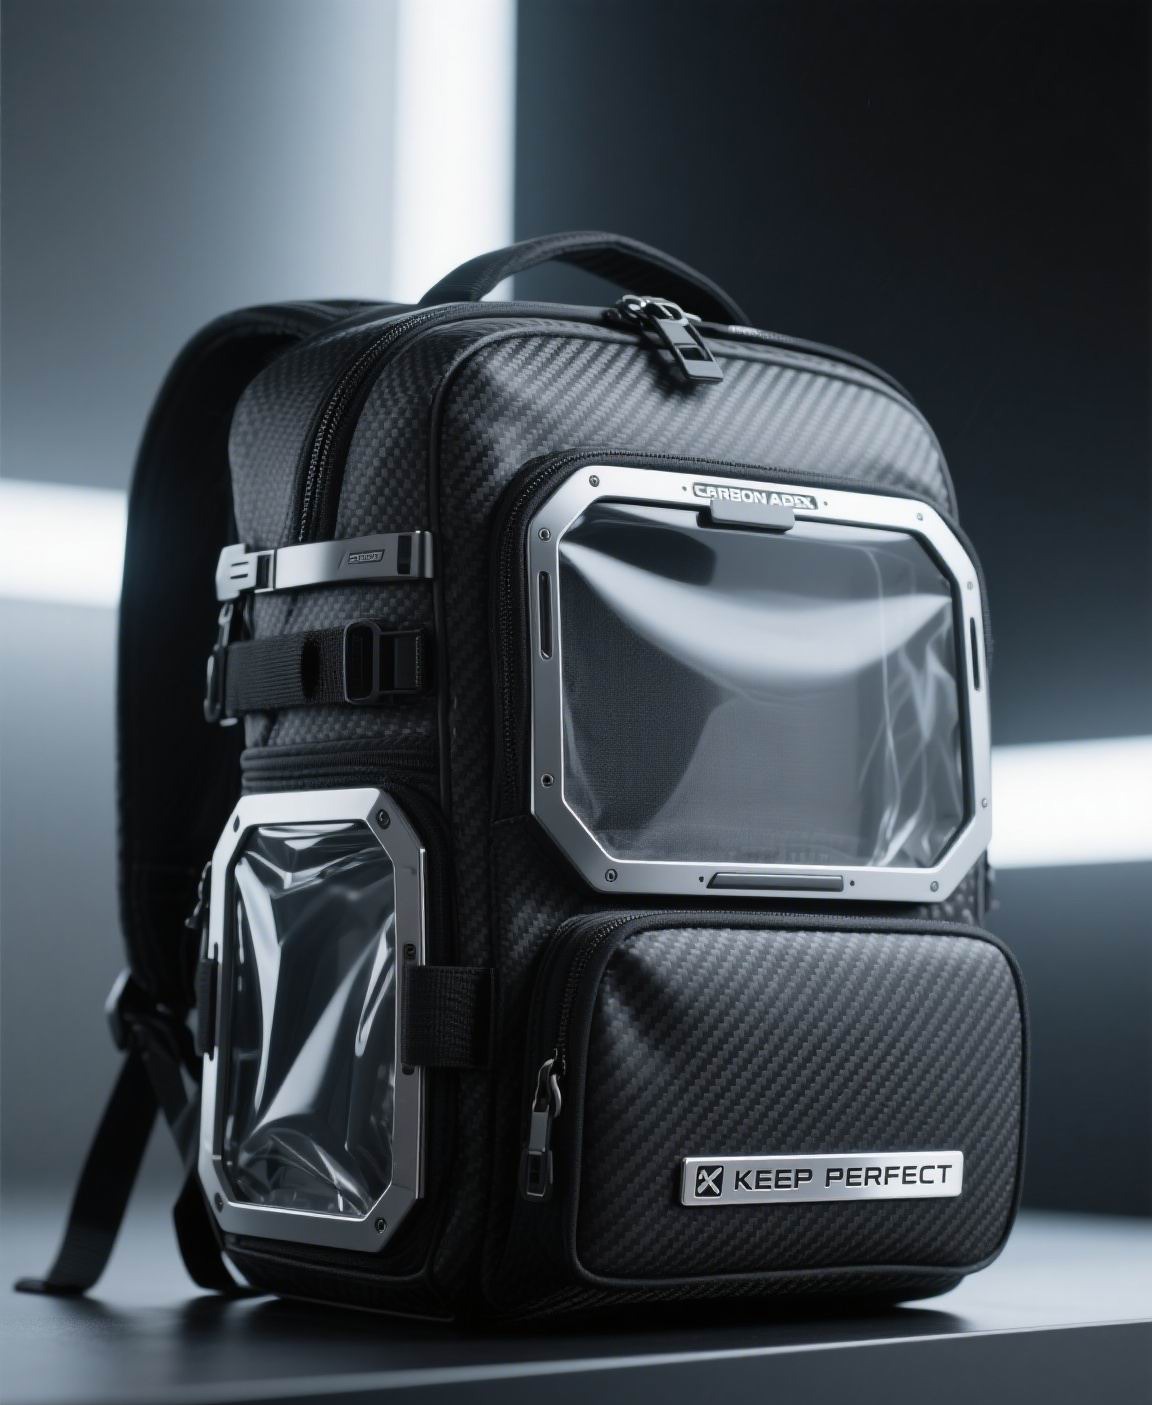
Unit cost for a custom modular bag system splits into two fundamentally different pools: a shared pool paid once for the carrier and its attachment interface, and a marginal pool paid per module. That split is why modular ranges look expensive at the first quote and cheap at the fourth season. Against MOQ 500, the non-recurring side is modest, sampling runs USD 50–150 and is refundable on order, and dedicated tooling or screens run USD 300–2,500. What actually decides the landed figure is hardware selection, reinforcement build-up, and how efficiently the packed carton fills a container. This breakdown walks each cost line in turn, the lever that moves it, and the risk that lever introduces when it is pushed further than the duty profile can absorb. It closes with the four-season arithmetic that shows exactly where a modular range stops looking expensive and starts looking cheap, and with the quotation inputs that produce a number which survives contact with the invoice.
Why modular cost behaves differently from monolithic cost
A monolithic backpack is priced as a single object; every cost line is charged once per unit and there is no shared infrastructure. A custom modular bag system carries an additional layer of cost that is not visible on the carrier itself: the interface. The interface includes the attachment field, the backing build-up behind each anchor, the tooling that makes the geometry repeatable, and the engineering time that defines the tolerance. All of that is paid once and then shared across every module that ever mounts to the platform.
This produces a distinctive cost curve. The first module is expensive because it carries the whole interface. The fifth module is comparatively cheap because it only adds fabric, thread, closures, and labour. A buyer comparing the first quote against a conventional backpack will see a premium; a buyer comparing total range cost across four seasons will usually see a saving, provided the interface was specified to the widest intended module from the start.
The practical consequence is that modular pricing cannot be judged per unit. It has to be judged per range, over the number of seasons the carrier is expected to stay in the catalogue. Buyers who evaluate a modular quote on first-unit cost alone consistently under-invest in the interface and then pay for it in module redesign.
There is also a working-capital dimension. A shared carrier allows inventory to be held at the platform level and configured late, which reduces the number of finished SKUs sitting in a warehouse. That saving does not appear on a quotation, but it often exceeds the interface premium within two seasons.
Bottom line: Cost a modular range across several seasons rather than per purchase order, because tooling written off against MOQ 500 during the first year becomes free capacity by the third.
The bill of materials, line by line
The bill of materials for a modular range is best read in four bands: substrate, interface hardware, closures, and finishing. Substrate covers face fabric, lining, and any foam or frame sheet. Interface hardware covers webbing, anchors, buckles, and backing components. Closures covers zips and sliders. Finishing covers binding, labels, print or embroidery, and packing. Each band behaves differently under volume and each band has a different failure consequence if reduced.
| Cost band | Typical share of unit cost | Primary driver | Reduction lever |
|---|---|---|---|
| Substrate | 30–40% | Fabric denier, coating chemistry, yield | Nest panels to raise marker yield |
| Interface hardware | 18–28% | Anchor type, plating, webbing grade | Reduce anchor count per module, not per carrier |
| Closures | 8–14% | Chain size, slider type, run length | Name YKK #5, #8, #10 by position |
| Labour | 15–22% | Bar-tack count, binding operations | Standardise reinforcement across modules |
| Finishing and packing | 6–12% | Branding method, carton efficiency | Compress cartons to protect container volume |
Marker yield on the substrate band deserves more attention than it usually receives. A panel layout that wastes eight percent of fabric costs more than a hardware downgrade saves, and unlike a hardware change it carries no functional risk. Ask for yield figures during sampling rather than at quotation, because yield is only knowable once the pattern is nested.
Hardware: where the money actually sits
Hardware selection is the single largest controllable decision in a custom modular bag system, and it is where branding intent collides with engineering reality. A magnetic-mechanical anchor costs substantially more per point than a standard side-release buckle, but it changes the user interaction completely: one-handed closure, self-locating alignment, and a premium tactile signal. A woven attachment field costs less per point but demands dimensional discipline and consumes more sewing time.
The cost trap is anchor count. Buyers frequently specify anchors at every conceivable position, then discover that half of them sit in zones the user cannot reach or does not need. Reducing anchor count per module reduces cost with no functional loss, while reducing anchor count per carrier reduces future flexibility. Those two reductions are not equivalent, and conflating them is the most common costing error in modular programmes.
Closures should be named by chain size rather than by how they look. Fit a #5 chain to pockets and module closures, step up to #8 where the main slider takes sideways force, and keep #10 for long runs on the biggest carriers. YKK is the default brand across all three. Naming the size prevents slider mismatch on the line, a defect that costs more to sort than the price gap between chain sizes.
Compliance carries its own cost line. Metal parts need nickel release testing to EN 1811, substance limits come from REACH (EC 1907/2006) at EU level and Prop 65 in California, and fabrics with trims are normally certified to OEKO-TEX Standard 100. Certified inputs cost more than untested equivalents, but the premium is far smaller than a recall or a rejected inbound shipment.
Takeaway: Pay for hardware carrying documented test evidence even at a premium, since failures spread across a monthly output of 200,000 units dwarf any saving between the two cheapest quotations.
Labour minutes and the operations that consume them
Labour in a modular build concentrates at three operations: webbing application, reinforcement bar-tacking, and binding. General assembly is comparatively predictable. Because reinforcement is both the durability mechanism and the cost driver, the engineering question is how much reinforcement is actually required at each position, which is answered by load testing rather than by habit.
A useful discipline is to classify every anchor into a load class and then assign a standard reinforcement build-up to each class. Three classes is usually enough: light, for modules under about half a kilogram; medium, for tool and utility modules; and heavy, for anything that swings or carries dense contents. Standardising build-ups across the range reduces operator variation, shortens changeover, and makes the cost model stable.
Binding and edge finishing is the second labour concentration, and it is the operation most often cut to save minutes. Cutting binding width saves seconds per unit and costs measurable durability at the edge, particularly on modules that are repeatedly pulled from a carrier. Where cost must come out of labour, take it from decorative topstitching rather than from edge protection.
Wash and care behaviour should be validated before the labour model is frozen. ISO 6330 domestic washing and drying cycles reveal whether a reinforcement patch curls or a binding tape shrinks relative to the face fabric, and a shrinkage mismatch discovered after the labour standard is set forces both a design change and a rate renegotiation.
Spec rule: Set labour minutes from a real operation breakdown before quoting, because a two-minute saving per unit across MOQ 500 outweighs every hardware substitution available afterwards.
Non-recurring cost and amortisation across MOQ 500
Two one-off figures matter in a modular programme. Expect a charge of USD 50–150 for samples, credited back once the order is placed. Dedicated tooling and print screens sit between USD 300 and 2,500, driven by whether a custom-moulded puller, a purpose-built buckle, or multi-colour printing is required. Both amounts are modest in absolute terms, and their real function is to force a decision: either commit to stock components or pay for differentiation.
Amortisation is straightforward arithmetic. Spread across MOQ 500, a USD 2,500 tooling charge adds five dollars per unit; spread across a three-season carrier run at several thousand units, it becomes negligible. This is the clearest argument for specifying the carrier interface once and reusing it, rather than re-tooling for each season is fashion change.
Sampling cost is best read as risk reduction rather than as a charge. A modular interface that has not been physically built has not been validated, and the cost of discovering a two-millimetre pitch error after mass production starts is orders of magnitude larger than USD 150. Buyers who request three sampling rounds almost always spend less in total than buyers who approve on the first photograph.
There is one further non-recurring item that buyers forget: testing. Abrasion work under ISO 12947 or ASTM D3884, water resistance under AATCC 127 or ASTM D751, and tensile work under ASTM D5034 are inexpensive individually and are the evidence base that prevents a downstream dispute about whether a defect was a material failure or a specification failure.
Verdict: Amortise screens, tooling and sample fees across the whole expected volume rather than the first drop alone, and require that amortisation schedule in writing before releasing any deposit.
Freight, duty and settlement arithmetic
Landed cost is where modular ranges either win or quietly lose. Pricing is quoted FOB Xiamen, so everything after the vessel sits on the buyer's own account. Freight mode is chosen by calendar: sea freight 25–35 days for planned replenishment, air 5–8 days for an announced launch, courier 3–5 days for samples and small replacement shipments. The cost difference between sea and air on a mid-volume order routinely exceeds the entire hardware premium discussed earlier.
| Option | Transit | Cost behaviour | Best used when |
|---|---|---|---|
| Sea freight | 25–35 days | Lowest cost per cubic metre | Replenishment against a known season |
| Air freight | 5–8 days | Charged on chargeable weight | Launch date already announced |
| Courier | 3–5 days | Highest per unit, simplest handling | Samples and replacement shipments |
| 20GP container | ≈28 CBM usable | Fixed cost per container | Order volume fills the box |
| 40HQ container | ≈68 CBM usable | Better rate per CBM when filled | Multi-SKU consolidated shipment |
Carton efficiency is the cheapest freight saving available. Plan on about 28 CBM inside a 20GP and roughly 68 CBM in a 40HQ; a modular set in oversized cartons can waste a fifth of the volume being paid for. Compressing the pack, or sending carriers flat with modules nested, usually buys more than any rate negotiation. Payment splits 30 percent on release of material and 70 percent once the inspection report is issued, with that inspection sampled to ISO 2859-1 at AQL 2.5.
Duty lines deserve primary sources instead of inherited rates: classification checked against exporter and market guidance published by trade.gov, with lot acceptance tied to a plan written to ISO 2859-1 at the agreed level.
Cost levers and the risk each one carries
Every lever that reduces unit cost transfers something. Downgrading face fabric transfers durability. Reducing anchor count per carrier transfers future flexibility. Cutting binding width transfers edge life. Removing reinforcement transfers load capacity, and it transfers it in the direction of the failure mode most likely to generate a return. The discipline is to choose the lever whose transferred risk the range can actually absorb.
The safest lever is yield improvement, because it costs nothing functionally. The second safest is SKU consolidation, because fewer module variants mean longer production runs and less changeover. The third is packing compression. These three together frequently deliver a larger saving than any component substitution, and none of them appears on the product as a visible compromise.
The most dangerous lever is unspecified substitution, where a supplier is asked to hit a price and left to choose how. That transfers the decision to whoever has the least information about the duty profile. Name the components, name the standards, and negotiate the price on the named build rather than on an abstract target.
One further lever deserves mention because it is frequently overlooked: order consolidation across seasons. Booking two seasons of carrier volume at once justifies a longer production run on our 4,950 m² SGS-verified production floor and avoids the re-setup cost that repeats when the same platform is reordered in small lots. Our production team can plan that run against 200,000 units per month of available output without crowding other programmes.
Writing a quotation request that gets an accurate answer
Quotation accuracy is a function of input quality. A request that states capacity, carrier dimensions, module count, attachment type, hardware preference, fabric denier and coating, branding method, quantity, and destination port will receive a figure that survives to invoice. A request that states a target price and a photograph will receive a number that changes after sampling, which is worse than no number because it anchors the buyer to a fiction.
State the duty profile in one sentence. Knowing whether the carrier is for daily urban commuting, field service, or weekend hiking changes fabric, reinforcement, and hardware selection more than any other single input, and it prevents the common failure where a range is priced for light duty and then sold for heavy duty.
State the compliance destination. CPSIA applies to certain categories in the United States, REACH (EC 1907/2006) applies in the European Union, California Prop 65 applies at state level, and OEKO-TEX Standard 100 or EN 1811 evidence may be requested by retail channels. Compliance inputs are cheaper when they are designed in than when they are retrofitted after a retailer asks.
Finally, state the timeline honestly. A programme with twelve months of runway can be built on stock hardware and sea freight; a programme with ten weeks cannot. Sharing the real constraint lets the production route be planned rather than improvised, and it is the single highest-value sentence in a quotation request. Start from the platform options shown under modular backpack architectures and current product platforms.
Total cost across four seasons: how the arithmetic actually works
The clearest way to judge a modular range is to model four seasons. In season one the buyer pays for the carrier platform, the interface engineering, tooling at USD 300–2,500, sampling at USD 50–150 refundable on order, and two or three modules. Unit cost looks high because every shared cost is amortised across a single season's volume. In season two the buyer pays only for new modules and a colour refresh, and the interface cost is already sunk.
By season three the comparison inverts. A conventional range has re-tooled at least once, because fashion pressure forces a pattern change, and each re-tool repeats sampling, pattern making, and operator familiarisation. The modular range has changed surface and content while holding geometry, so its incremental cost per season is a fraction of the conventional equivalent. Buyers who model this properly almost always conclude that modular is cheaper, and the crossover usually lands in the second or third season.
The model has three assumptions that must hold. First, the carrier geometry must stay stable, which is a design commitment rather than a supplier commitment. Second, the interface must have been specified to the widest intended module, or a season-two accessory will not fit and the platform has to be reworked. Third, volume must be sufficient to justify the platform: below a few thousand carriers across the range, the shared cost does not amortise and a conventional build is genuinely cheaper.
Where the model fails, it fails for identifiable reasons. The most common is a mid-life interface change driven by a single large customer request. The second is fabric substitution that changes thickness enough to alter how a reinforcement patch behaves, which is a hidden interface change even though the drawing did not move. The third is a module that was designed against a competitor's field rather than the frozen interface, which produces fit complaints that look like quality problems but are specification problems.
Handled well, the four-season view also improves negotiating position. A buyer who can commit to carrier volume across three seasons can ask for a longer run on our 4,950 m² SGS-verified production floor, and a longer run means fewer changeovers, tighter tolerance consistency, and fewer dye-lot mismatches between carrier and modules. That is a cost saving that never appears as a line item but shows up in return rates.
Judgement: Score candidates on four-season total cost including re-validation, inspection and freight rather than on the FOB Xiamen unit price printed on the first quotation.
Frequently asked questions
Why does a modular range cost more than a conventional backpack at first quote?
The carrier carries the interface cost: attachment field, backing build-up, and tooling. That cost is shared across every later module, so the first unit looks expensive while the fifth season looks cheap. Judge a modular range per range over its catalogue life, not per first unit.
What are the non-recurring costs in a modular programme?
Sampling runs USD 50–150 and is refundable against the order. Tooling or print screens run USD 300–2,500 depending on whether a moulded puller, bespoke buckle, or multi-colour screen work is needed. Testing is additional and modest.
How does MOQ 500 affect the amortised cost?
Against MOQ 500, a USD 2,500 tooling charge adds roughly five dollars per unit. Spread across a carrier run that continues for three seasons, the same charge becomes immaterial. This is the argument for specifying the interface once and reusing it.
Which cost lever is safest to pull?
Marker yield improvement is safest because it costs nothing functionally, followed by SKU consolidation and carton compression. Together these often deliver more than any component substitution, and none appears on the product as a visible compromise.
How much does hardware selection move unit price?
Interface hardware accounts for roughly 18–28% of unit cost. A magnetic-mechanical anchor costs substantially more per point than a side-release buckle, and reducing anchor count per module lowers cost without removing carrier flexibility.
How should zips be specified to control cost?
Name chain size by position: YKK #5 for module closures and pockets, YKK #8 for main access where the slider sees lateral load, YKK #10 for long runs on large carriers. Naming by size prevents slider mismatch, which costs more to sort than the price gap.
What freight mode gives the lowest landed cost?
Sea at 25–35 days gives the lowest cost per cubic metre and suits planned replenishment. Air at 5–8 days is for an announced launch, and courier at 3–5 days handles samples. Moving from sea to air often costs more than the whole hardware premium.
How much container volume should a modular order plan for?
Around 28 CBM fits inside a 20GP and about 68 CBM in a 40HQ. Carton efficiency beats rate negotiation: oversized cartons waste up to a fifth of the space paid for, so compress the pack or nest modules before booking.
What payment terms apply and when is the balance due?
Terms are 30 percent up front to release material and reserve the line, then 70 percent once the inspection report clears. Prices are quoted FOB Xiamen, leaving freight and destination charges to the buyer.
Which compliance costs should be budgeted from the start?
Allow for EN 1811 nickel release testing on metal parts, substance compliance with REACH (EC 1907/2006) and California Prop 65, OEKO-TEX Standard 100 on fabrics and trims, and CPSIA evidence where the market and product category demand it.
How does labour cost concentrate in a modular build?
Labour concentrates at webbing application, reinforcement bar-tacking, and binding. Classify anchors into light, medium, and heavy load classes and assign one standard reinforcement build-up per class to reduce operator variation and stabilise the rate.
Can reinforcement be reduced to hit a price target?
Reinforcement can be reduced only where load testing supports it. Removing it transfers risk directly into the failure mode most likely to generate a return. Take cost from decorative topstitching rather than from edge protection or backing build-up.
Does ordering two seasons at once reduce cost?
Yes. A longer run avoids repeated setup and changeover and can be planned against our 4,950 m² SGS-verified production floor without crowding other programmes. It also stabilises dye lots across the carrier and its modules.
What makes a quotation request accurate?
State capacity, dimensions, module count, attachment type, hardware preference, fabric denier and coating, branding method, quantity, destination port, duty profile, and real timeline. A target price plus a photograph produces a number that changes after sampling.