Home › Field notes › DTC Brands and Modular Bags: SKU Economics, Cash and Launch Gates
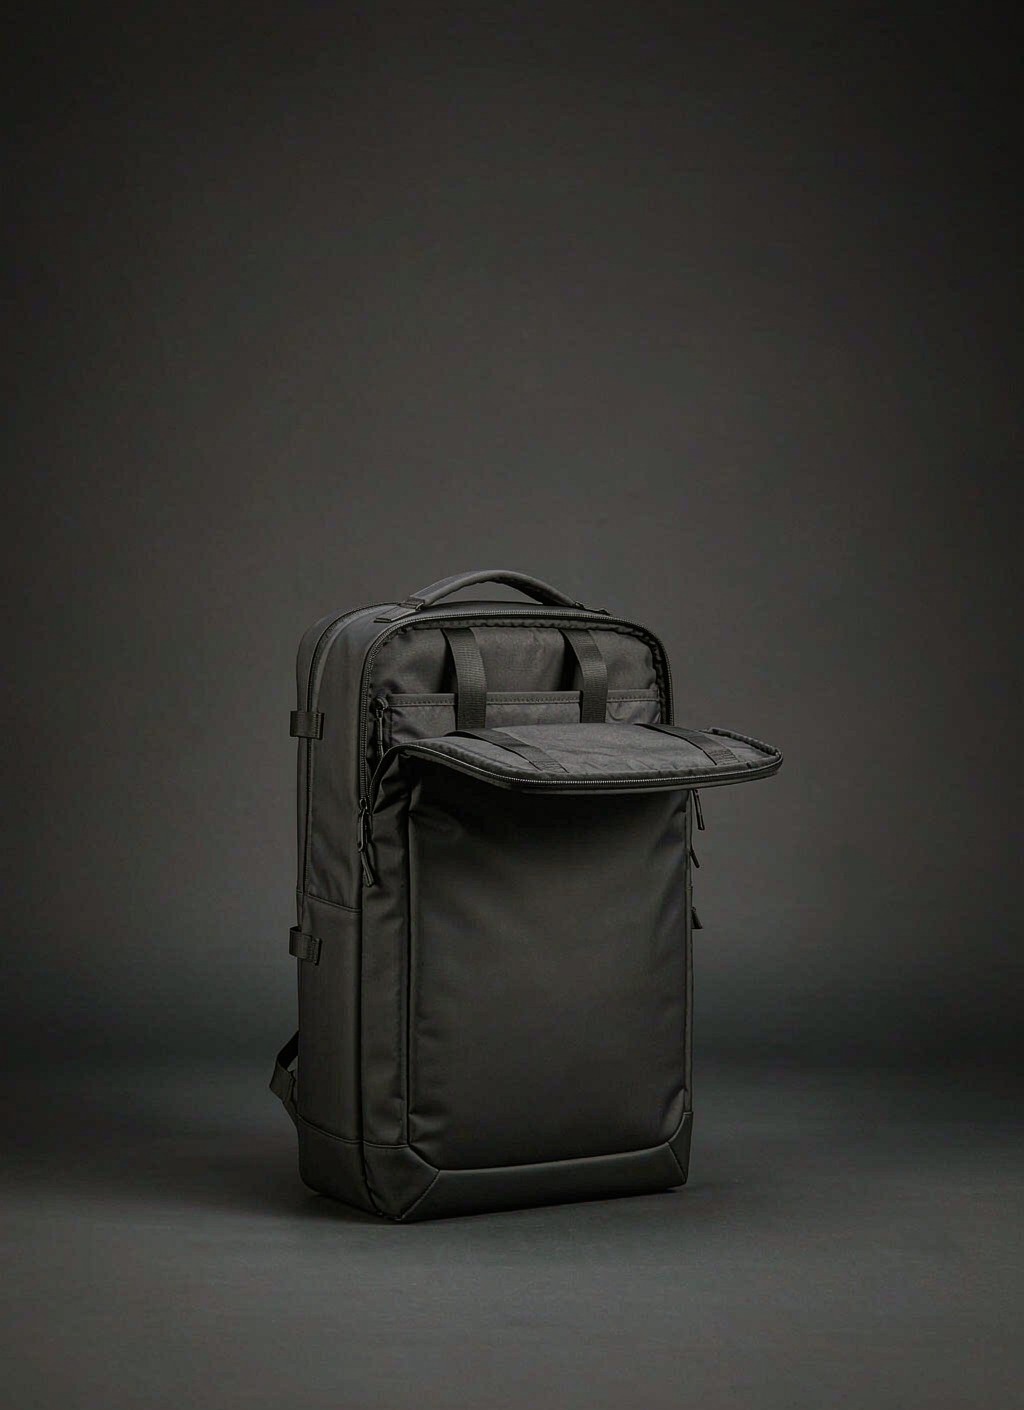
Modular bags suit a direct-to-consumer label because they turn one certified chassis into a catalogue rather than a single listing. A body that accepts five or six attachable modules gives the merchandising team more pages, more bundles and more reasons to email, while the factory sees one shell and one interface to control. The economics start with MOQ 500 per module variant and sampling 6-10 working days per new part, and they hold only if the interface stays frozen between seasons. Where a conventional catalogue buys breadth by buying more finished products, a modular catalogue buys breadth by buying more small parts against a body that is already paid for. Everything that follows is written for the operator who signs the purchase order rather than the one who chose the colourway, and the comparison below costs both structures on the lines that actually appear in the accounts: development spend, inventory positions and content units.
Where a conventional DTC catalogue runs out of oxygen
The failure pattern for a young bag label is rarely demand. It is the shape of the inventory. Each new silhouette is a new pattern, a new material buy, a new sample round and a new minimum, and each one lands as finished goods that have to be sold in a colour and a size the customer happened to want. Four silhouettes in three colourways is twelve inventory positions before a single accessory exists, and the cash in those positions is illiquid for as long as the listing underperforms.
The second constraint is attention. A listing needs photography, copy, a size or capacity story, review seeding and paid traffic to become visible. Spreading the same monthly content budget across twelve listings produces twelve weak pages. The same budget against three listings produces three pages that rank, convert and generate the reviews that finance the next launch.
Modularity attacks both constraints in the same move. The chassis is the expensive, slow, capital-heavy part of the programme and it is bought once. The modules are cheap, quick and small, and they multiply the number of things a customer can buy without multiplying the number of bodies in the warehouse. The trade-off is discipline: the interface has to stay fixed, or the accessory roadmap silently becomes a set of incompatible one-offs that nobody can merchandise.
A third constraint appears once volume grows: production capacity is booked by product, not by brand. A factory planning a season allocates lines to complete items with a known cycle time, and a late addition competes for a slot that is already promised. A modular programme behaves better here, because a small accessory run can be squeezed between larger bookings in a way a full silhouette cannot, and because the body run is planned months ahead against a forecast rather than against a launch.
Bottom line: Move to a chassis-and-module catalogue once SKU complexity outruns forecast accuracy and not before, because modularity adds a documentation load that a small team must carry at MOQ 500 per component.
The chassis-and-module model, costed out
Put the two structures side by side before committing. A conventional programme treats every listing as a complete product; a modular programme treats the body as a platform and the listing as a configuration. The table below is written as the account would see it: development spend, inventory positions, content units and the re-order flexibility that follows.
| Cost line | Four separate silhouettes | One chassis plus five modules | Where the difference lands |
|---|---|---|---|
| Pattern and sample rounds | Four full rounds | One body round, five small rounds | Development calendar, not unit price |
| Inventory positions at launch | Twelve or more | One body, five accessory lines | Working capital tied up before first sale |
| Content units to produce | Four full shoots | One full shoot, five short ones | Monthly studio and editing budget |
| Re-order flexibility | Whole product, whole minimum | Single module, small minimum | Ability to chase a bestseller |
| Risk if one item misses | Finished goods written down | Small part, reused next season | Size of the mistake |
The last two rows are why operators adopt the model. Re-ordering a single module that is selling out is a small purchase against a frozen drawing; re-ordering a finished silhouette is a full production slot and a full freight decision. And when a module misses, the loss is a small part with a short run rather than a container of finished bags that has to be discounted.
Read the comparison honestly, though. A modular catalogue only pays if the attach rate is real. If the average order contains one module, the model has added complexity without adding revenue, and the correct response is to fix merchandising rather than to add more parts.
Verdict: Cost the platform as one body plus reusable modules rather than as separate products, since that structure is where cash, storage and photography savings appear once the first 500-unit body run is booked.
Cash: deposits, inventory risk and the re-order curve
Payment structure sets how much of the year the money is tied up. T/T 30/70 is the standard arrangement: thirty percent to release materials and book the line, seventy against documents before the container sails. For a first programme that means the deposit leaves months before revenue arrives, and the size of the deposit is set by the size of the first run, which is set by the minimum. MOQ 500 is the working floor for a module programme, and it applies per variant, so five colourways of the same pouch is five minimums unless the order is consolidated against one material buy.
The sensible first move is to consolidate colour, not to reduce quantity. One colourway of each module at a workable quantity gives a clean read on demand; three colourways at a third of the quantity each give three half-answers and three re-order decisions at once. Once the attach-rate data exists, colour can be added against evidence rather than against optimism.
Book the re-order calendar before the first container sails. Fabric and hardware lead times, not sewing time, are what stretch a re-order, and the hardware is usually the long pole because a closure family in a specific colour is a purchased part with its own minimum. Order the second run's hardware with the first run's fabric wherever the forecast supports it; the carrying cost of a box of buckles is trivial next to a stockout in the middle of a paid campaign.
Takeaway: Reserve working capital for hardware rather than finished goods, holding buckles and webbing against a 6-10 working days sampling need instead of locking cash into boxed inventory.
Freight, dimensional weight and landed cost
Two freight facts decide whether a module programme is profitable. The first is the quoted basis: FOB Xiamen, meaning the price covers goods and origin handling, and everything after the rail of the ship is the buyer's problem. The second is the mode, and the spread between modes is wide enough to change the plan. Sea freight 25-35 days is the default and the cheapest per unit. Air 5-8 days is the rescue when a launch date is at risk. Courier 3-5 days is for samples and for small top-ups where speed matters more than cost per piece.
Modules are light and bulky, which is the worst possible profile for air freight, where dimensional weight governs the bill. That asymmetry is worth designing around: a pouch that ships flat and fills out in use costs less to fly than one with a fixed moulded shape, and a packaging card that folds flat rather than a rigid box saves real money across a season of air shipments.
Container planning is where the two structures diverge again. Plan against 20GP around 28 CBM and 40HQ around 68 CBM, and remember that a modular programme ships mixed cartons: bodies, pouches and packaging cards in the same container. Mixed cartons pack well if the carton spec is fixed early, and badly if every part arrives in its own bespoke box. Fix one master carton specification per programme and let the parts share it.
Then finish the landed-cost model honestly. Duty, inland delivery, marketplace fulfilment fees and the cost of a return all sit outside the FOB number, and a modular programme changes two of them: fulfilment, because a module ships as a small parcel, and returns, because a part can come back on its own. Model both before the first price is published, because a bundle price set without the fulfilment line is a margin decision made by accident.
Cross-border paperwork deserves sources rather than guesses, so check destination requirements against exporter and market guidance published by trade.gov while bundles are still being priced rather than during clearance.
Returns, reviews and the attach-rate loop
A modular catalogue generates a data asset that a conventional catalogue cannot: attach rate. Because modules are separate lines, the order data shows which combinations sell, which module is bought as a second purchase, and which bundle is returned. That is the signal that should drive the next development round, and it is cheap to capture if the SKU structure was designed for it rather than inherited from a spreadsheet.
Returns behave differently too. A modular order can be partially returned, which lowers the cost of a mistake, but it also means the return reason attaches to a part rather than to a product. That is useful: "pouch too small for a large phone" is actionable in a way that "bag not as expected" is not. Route return reasons into the tech pack review, and treat any reason that appears more than a handful of times in a quarter as a specification change, not as a customer service issue.
Reviews deserve their own plan. Modular products invite a specific kind of review - the configuration photo - and those photographs sell the platform better than studio images do. Ask for them explicitly in the follow-up email, sequence the ask after the customer has had the product long enough to configure it, and feed the most common configurations back into the default bundles on the product page.
Content cost: what each listing actually consumes
Content is the hidden minimum of a consumer catalogue. Every listing needs a hero image, a scale reference, a capacity demonstration, and a short piece of motion for the paid channels. Producing that for a full silhouette is a studio day; producing it for a module against an existing chassis is an hour, because the chassis shots already exist and the module only needs to be shown attaching and in use.
| Asset | New finished silhouette | New module on an existing body | Reusable next season |
|---|---|---|---|
| Hero stills | Full studio day | Add-on set against existing chassis shots | Yes, if interface unchanged |
| Capacity demonstration | New pack-out sequence | Single insert shot | Yes |
| Motion for paid | Full edit | Short clip reusing body footage | Yes, with recut |
| Interface explanation | Not applicable | Close-up of the attachment action | Yes, the core reusable asset |
| Review seeding units | Whole product per reviewer | One module per reviewer, body already held | Partly |
The interface explanation asset is the one to over-invest in. It is the piece that answers the objection behind every modular purchase - will this actually attach to what I already own - and it is reusable across every module you ever release on that interface. Shoot it once properly, in a single frame that shows the hands, the hardware and the row alignment, and the whole catalogue inherits it.
Quality gates that protect a young label
A young brand does not survive a season of defects, because it has no review history to absorb them. The gate that matters most is the pre-shipment inspection, and the standard working level for sewn goods of this class is AQL 2.5 with the sampling plan drawn from ISO 2859-1. Write the defect classification into the same document: critical for anything that affects safety or releases unintentionally, major for dimensional drift or broken interchangeability, minor for appearance inside a stated viewing distance.
The second gate is the golden sample, and it is where most arguments start. Approve one sample, sign it, keep it, and reference it in the purchase order by sample number and date. Anything the bulk does not match is then a deviation from a signed reference rather than a difference of opinion. Ask for the bulk to be built from production-intent materials with the production hardware, not from whatever was on the shelf when the sample was cut, because hardware substitution is the most common silent change in soft goods.
Third, hold a first-article check at the line before bulk cutting starts. It costs one day and catches the class of error that inspection cannot: a closure placed 4 mm off, a label in the wrong language, a webbing width that reads 25 mm on the drawing and 24 mm on the roll. Nothing downstream of that check is cheap to fix.
Finally, decide in advance what happens to a failed inspection. A defined remedy - rework at the supplier's cost, a second inspection, or a short-shipment against a credit - removes the negotiation that otherwise eats the launch window. Write it into the purchase order next to the sampling plan, so both sides know the consequence before the cartons are packed rather than after.
Spec rule: Write defect definitions before inspection rather than afterwards, agreeing the AQL 2.5 level in advance so a young label pays once for a bad batch rather than twice.
Compliance before the first listing goes live
Marketplace and retail channels will ask for documentation before they ask for product, and the list is short and predictable. REACH (EC 1907/2006) declarations cover the EU. California Prop 65 warnings apply where a listed substance is present above a safe-harbour level. CPSIA documentation, including tracking labels, applies to anything presented as a children's product. OEKO-TEX Standard 100 on the fabrics shortens most European retailer conversations.
Ask for the documents at quotation stage, not at shipment. A test report produced in a hurry is the most expensive document in the programme, and a certificate whose scope does not cover the actual assembly is worse than none because it fails at the buyer's own audit rather than at yours. Check three things on every certificate: the number, the scope statement and the date. Then file the translated declarations with the listing data so the marketplace onboarding team never has to ask twice.
Consumer listings lean on third-party evidence, keeping textile claims inside OEKO-TEX Standard 100 boundaries and translating declarations into the language each marketplace actually reviews.
A ninety-day launch sequence with the gates named
Sequence matters more than speed. The first thirty days go to the brief and the drawing: interface frozen, materials chosen, closure specified with numbers, and the target landed cost written down against FOB Xiamen. Nothing should be sampled until the interface drawing is signed, because every later change to it voids every module quoted against it.
The middle thirty days are sampling and content. A straightforward module samples in 6-10 working days, a complex one in 12-15, and the sample charge of USD 50-150 is credited back when the order is placed. Screens and tooling sit at USD 300-2,500 where a custom part, a woven label or a printed pattern is involved. Photograph the approved sample for the interface asset in the same session, so the reusable footage exists before the launch date is fixed.
The final thirty days are production and freight. Mass production 35-50 days, T/T 30/70 with the deposit releasing materials, inspection at AQL 2.5 before the balance is paid, then sea freight 25-35 days or air 5-8 days if the date has slipped. Build the container plan against 20GP around 28 CBM and 40HQ around 68 CBM at the same time as the order, not after the goods are packed.
Judgement: Sequence ninety days as prototype, then 35-50 days of bulk, then either 25-35 days at sea or 5-8 days by air, and publish the closing date of every gate before the first deposit moves.
Frequently asked questions
Why do modular systems suit direct-to-consumer brands more than wholesale?
Because the channel rewards listing depth and fast re-orders, both of which a modular structure delivers cheaply. A wholesale buyer wants one finished product per line review; a consumer storefront rewards bundles, add-ons and configuration stories. The same interface supports all of them without new tooling.
What minimum quantity should a first module order be?
Plan against MOQ 500 per variant and consolidate colour rather than splitting quantity. One colourway at a workable quantity gives a clean demand read; three colourways at a third each give three partial answers and three re-order decisions at the same time.
How long does sampling take for a new module?
A straightforward pouch samples in 6-10 working days; a build with a moulded part, a custom closure housing or a printed pattern runs 12-15. The sample charge of USD 50-150 is credited back against the order, so the real cost of a slow sample round is calendar time, not money.
What does tooling and artwork setup cost?
Screens, dies and small tooling land at USD 300-2,500 depending on whether a moulded component is involved. Woven labels and printed panels sit at the lower end, moulded parts at the upper. Budget it as development spend and amortise it over the planned run, not as part of unit price.
How should a young label structure payment?
T/T 30/70 is standard: thirty percent releases materials and books capacity, seventy settles against documents before sailing. FOB Xiamen is the quoted basis, so freight, duty and inland delivery sit with the buyer and must be in the landed-cost model from the first spreadsheet.
Which freight mode should a launch shipment use?
Book the season on sea transit of 25-35 days; reserve air at 5-8 days for a deadline that genuinely cannot move, and use courier at 3-5 days for samples and replenishment parcels. Accessories are bulky relative to their mass, so air invoices follow dimensional weight and hurt more than the unit margin suggests.
How much working capital does a modular catalogue free up?
The saving is in inventory positions, not in unit price. One body plus five modules is six purchase lines and one large one, against twelve or more finished-goods positions for a four-silhouette range. The freed cash is the difference between those two inventory positions at any point in the season.
What inspection level should a consumer brand require?
AQL 2.5 with the sampling plan taken from ISO 2859-1, and defect classes defined in the same document. Classify unintended release as critical, dimensional drift that breaks interchange as major, and appearance issues inside a stated viewing distance as minor.
How is attach rate used in development planning?
Read it from order lines, not from surveys. Which module sells with which body, which is bought as a second purchase, and which bundle is returned most often. Any return reason appearing more than a handful of times in a quarter should become a specification change.
Do modular products complicate returns handling?
They reduce the cost of a mistake because an order can be partly returned, and they improve the data because the reason attaches to a part. "Pouch too small for a large phone" is actionable; "bag not as expected" is not. Route reasons into tech pack review.
Which compliance documents must exist before listing?
REACH (EC 1907/2006) declarations for the EU, California Prop 65 warnings where listed substances are present above safe-harbour levels, CPSIA documentation with tracking labels for children's items, and OEKO-TEX Standard 100 on fabrics for most European retail conversations.
Should a brand freeze the interface across seasons?
Yes, and treat any change as a re-validation event. Frozen interface dimensions are what let this year's module fit last year's chassis. An unrecorded change to webbing width or row pitch surfaces as a one-star review rather than as a defect report.
What container plan should a launch season assume?
Plan mixed cartons against 20GP around 28 CBM and 40HQ around 68 CBM, and fix one master carton specification per programme so bodies, pouches and cards share it. Bespoke cartons per part pack badly and raise freight per unit.
When should hardware be re-ordered?
With the fabric of the preceding run wherever the forecast supports it. Closure families in specific colours are purchased parts with their own minimums and the longest lead time in the bill of materials, while the carrying cost of a box of buckles is trivial next to a stockout.