Home › Field notes › Interchangeable Compartments: The Next Phase of Backpack Design
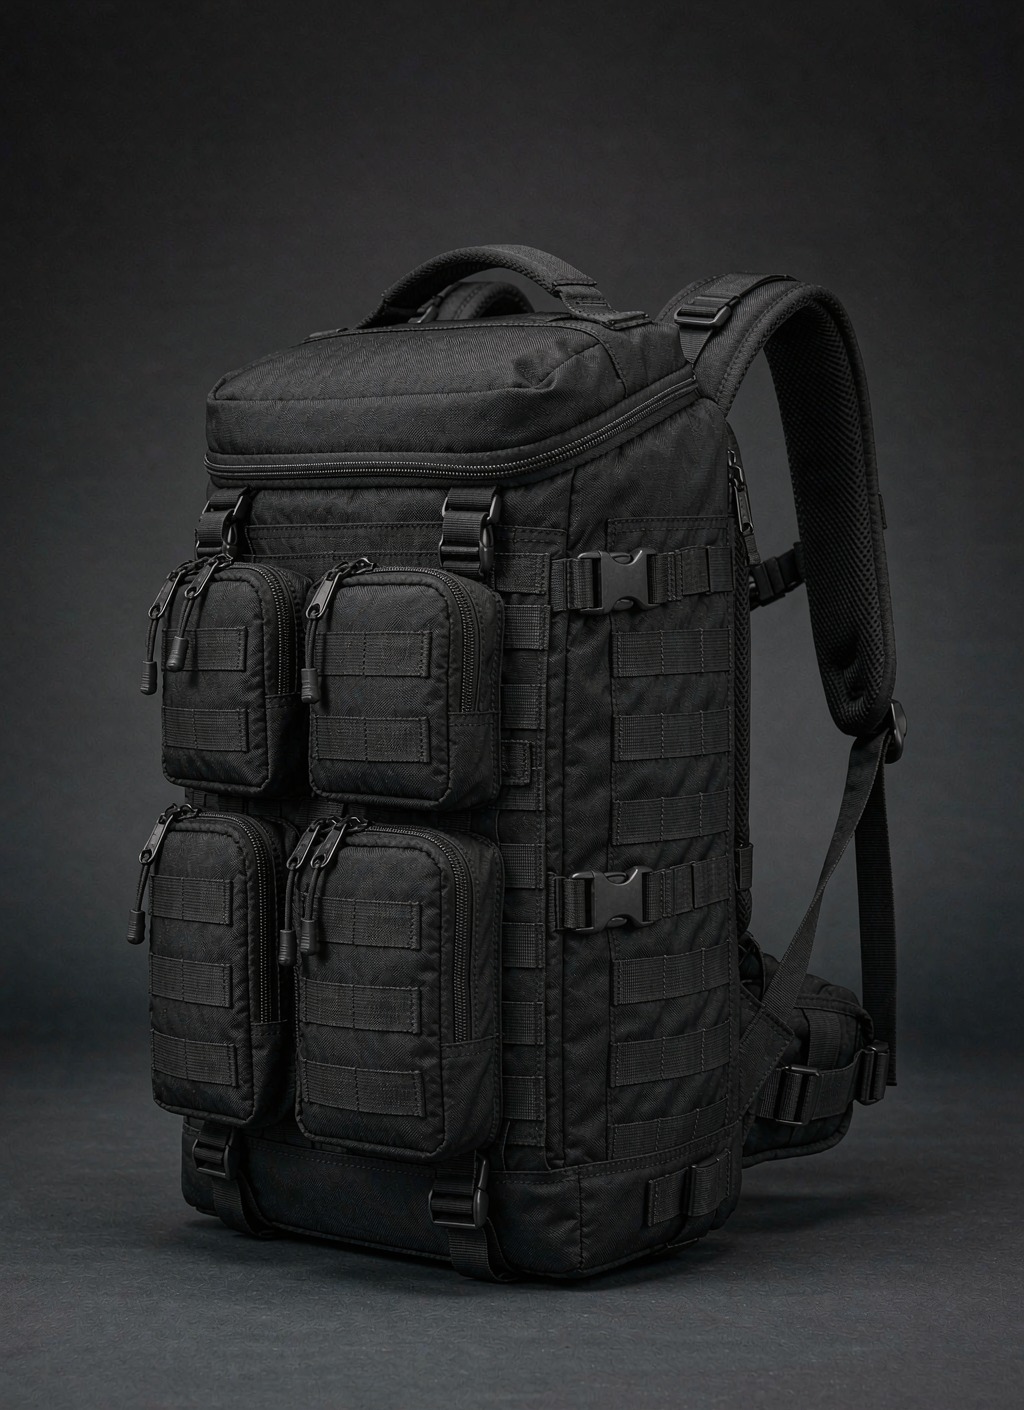
Interchangeable compartments change what a buyer is purchasing: not a container of fixed capacity but a chassis whose internal configuration is decided after the sale, by the user, repeatedly. That shift has a design consequence and a commercial one. The design consequence is that the load path can no longer be engineered for one known content set, because the content set is now a variable. The commercial consequence is that a range can be expanded by adding modules rather than silhouettes, which is cheaper and faster - sampling a module is a smaller job than sampling a body, and both run in 6-10 working days for standard work. This article sets out the three-layer model, the interface discipline it requires, and the conditions under which the modular thesis stops paying.
From Fixed Volume to Re-Specifiable Capacity
A conventional backpack is specified by its volume and its pocket count, and both are settled at design. A modular backpack is specified by its chassis envelope and its interface, and the pocket count becomes a variable the user sets each morning.
That is a different kind of product and it fails differently. A fixed-volume pack is optimised for a notional content set; when the user's contents diverge from that set, the penalty is inefficiency rather than failure. A modular pack is optimised for reconfiguration; when the interface drifts or the anchor is under-reinforced, the penalty is a module detaching under load, which is a return rather than a complaint.
The design response is to move the engineering effort from the interior to the interface. Interior layout can be left to the user because the user is better at it; the anchor geometry, the reinforcement extent and the retention value cannot be left to anyone, because those are the parts that fail when they are wrong.
The commercial response is to treat the module range as a portfolio with its own economics rather than as an accessory list. That portfolio has a correct size, and sizing it wrongly is the most common way modular programmes lose money - covered in its own section below.
There is also a user-behaviour assumption buried in the idea, and it should be stated rather than assumed. Interchangeability only creates value if the user's contents actually change: a commuter who carries the same laptop, the same cable set and the same lunch container every day gains nothing from a reconfigurable interior beyond the initial setup. The value concentrates in users whose day changes - field staff, hybrid workers, travellers moving between city and trail - and a range should be aimed at them explicitly rather than at everyone.
That targeting has a specification consequence worth noting. Users whose day changes tend to carry harder objects - tools, devices, wet kit - which pushes the module mass class up and makes the anchor reinforcement the deciding feature. Aiming at a static-content user would let the same chassis be built lighter, and building it light and then selling it to a changing-content user is how modular ranges acquire a return problem.
Selection rule: Size the chassis envelope for users whose contents change every few months, because optimising static volume for a changing-content owner produces the same return problem as narrowing the 38 mm vertical spacing for cosmetic reasons.
The Three-Layer Model: Chassis, Interface and Module
Modular products are easier to reason about as three layers with different rates of change. The chassis changes rarely, the interface should not change at all, and the modules change constantly. Most modular failures are a violation of that rate structure.
| Product layer | Intended rate of change | Failure when the rate is violated |
|---|---|---|
| Chassis | Every few seasons | Modules designed for the old body stop mounting |
| Interface | Never within a platform | Gradual incompatibility across the module family |
| Module | Every season | Stale range, no newness for the accessory buyer |
The middle row is the one that carries the value. A frozen interface is what allows a module designed in one season to mount in the next, which is what turns a set of accessories into an ecosystem. An interface that moves - even slightly, even for a good reason - resets that accumulated value to zero.
Practically, freezing an interface means publishing three callouts and refusing to negotiate them: a 25 mm webbing width, a 38 mm vertical spacing and a 50 mm horizontal repeat, each with a stated tolerance. Those numbers are not aesthetic. They are what make a pouch from another maker thread the field, and they are the reason the geometry survived while competing interfaces did not.
Verdict: Freeze the interface at 25 mm webbing width with 38 mm vertical spacing and 50 mm horizontal repeat, then let chassis and modules change around it, since capacity can be revised later while a narrowed pitch cannot be undone.
Interface Stability as the Design Asset
The instinct of most product teams is to improve the interface each season. That instinct is correct for every part of a bag except this one, and the reason is that the interface's value is a function of its stability rather than its quality.
Consider what a stable interface buys. Third-party accessories mount without permission. Modules from earlier seasons keep working, which makes the accessory purchase feel safe. Retailers can merchandise a pouch against a chassis without checking compatibility. And the brand can add a module in a single season without re-testing the platform.
Now consider what an improved interface costs. Every existing module has to be re-checked. Retailers have to re-merchandise. Users with the previous generation discover that the new pouch does not fit the bag they bought last year, and they discover it at the point of sale rather than in a specification. The improvement has to be substantial to pay for that, and it rarely is.
The defensible position is to freeze the geometry and compete on everything else - module design, materials, hardware feel, and the quality of the anchor. Those are open to improvement without invalidating anything already sold. Where a genuine improvement to the interface is unavoidable, the honest route is a new platform generation with a published cut-over, not a quiet change inside an existing one.
One practical mechanism helps: publish the interface as a standalone document rather than as a note inside a chassis drawing. A standalone interface sheet can be referenced by every module in the range, can be issued to third parties making compatible accessories, and makes a proposed change visible to everyone at the moment it is raised instead of after it has been built.
Bottom line: Publish the interface geometry so accessory makers can build against it, holding the 25 mm tape width and the 50 mm horizontal repeat constant even while chassis styling changes every season.
Sizing the Module Portfolio
Modules are cheaper to develop than chassis, which makes it tempting to launch many. The constraint is not development cost; it is that each module consumes a configuration minimum, a forecast, and shelf or warehouse space, and that unsold module stock is harder to liquidate than unsold chassis stock because it is only useful to someone who already owns the platform.
| Portfolio size | Development load | Inventory exposure |
|---|---|---|
| Three to five modules | Low, one sampling round | Concentrated, each line forecastable |
| Six to ten modules | Moderate, staged releases | Spread, with clear winners and losers |
| Eleven or more | High, continuous sampling | Diffuse, long tail ties up working capital |
Each configuration carries its own material call-off and sewing setup, and MOQ 500 per configuration is the working level. A portfolio of ten modules therefore commits as much setup capacity as a chassis programme ten times over, which is why the correct launch size is usually smaller than the design team's list.
The better sequence is to launch with the modules that have a clear use story - a laptop or device sleeve, a toiletry or wash module, a tool or cable organiser - and add the speculative ones only after a season of sales data. Sampling is 6-10 working days, so a module can be added quickly when demand is demonstrated rather than guessed.
A second filter helps before anything is committed: each proposed module should be able to name the object it carries and the situation in which it is carried. A module described as a general organiser usually fails that test and usually sells accordingly. One described as carrying a specific tool, device or wash kit to a specific place has a use story, and a use story is what turns a specification into a purchase.
Takeaway: Add modules only where each one carries a use story naming the tool, device or wash kit it moves and where it moves it, because the chassis must still ship economically at MOQ 500 per configured version.
Load Path and Structural Consequences
Modularity moves load away from the places a conventional pack is designed to carry it. A conventional pack transfers contents into the panel through a lining and a base; a modular pack transfers them through an anchor row, at a point, often with a lever arm.
Three consequences follow. The first is that the anchor row needs reinforcement whose extent is dimensioned rather than assumed. A reinforcement that stops at the stitch line does nothing, because the failure is the fabric tearing just beyond it. Stating the reinforcement extent as a dimension on the drawing, measured beyond the last stitch, is the control, and it is the field most specification sheets omit.
The second is that the module contents need a stated mass class. Without one, the heaviest object a user can imagine ends up in the module, and the anchor is then judged against a load nobody specified. Stating a mass class per row converts an unbounded risk into a bounded one and gives the inspector a rule.
The third is that the chassis has to tolerate asymmetric loading. A conventional pack is packed roughly symmetrically; a modular pack can have one heavy module on one side and nothing on the other. That asymmetry produces a torsional load through the frame sheet and the harness, and it is the reason modular chassis benefit from a stiffer back panel than a conventional equivalent of the same volume. Where a chassis is used across several configurations, the modular work backpack notes cover the reinforcement scheme in more detail. Inspection should reflect the same priority: sampling taken from ISO 2859-1 at AQL 2.5 is standard practice, but the anchor row warrants a check applied to every unit rather than to a sample, because it is the one feature whose failure produces a detached module rather than a cosmetic complaint. Agreeing that extra check at the same time as the sampling plan costs nothing; adding it after the first return costs a specification revision.
Judgement: Extend the anchor-row check agreed for sampling to every module that shifts load outward over the 25 mm interface row, since a module detaching under load defeats the reason for carrying it externally.
Manufacturing and Inventory Consequences
On the production side, modularity trades pattern work for planning work. One chassis pattern supports the whole range, so pattern development cost falls; in exchange, the number of distinct stock-keeping units rises and the forecasting problem becomes a two-part one.
The production window behaves well. Mass production of 35-50 days can cover a release containing several modules rather than a single body, because the chassis operations are common and the modules are smaller jobs running alongside. The calendar risk moves earlier, to material call-off and interface hardware availability, which is where modular programmes are usually won or lost.
Inventory behaves differently again. Chassis and modules can be held separately, which is a genuine advantage: unsold module stock does not strand a complete finished good. But module demand has to be forecast against chassis sales rather than as independent items, and the ratio is not stable - it changes as the installed base of chassis grows and as new modules are introduced.
The error to avoid is forecasting modules as a percentage of chassis units in the launch season. Early buyers purchase more modules per chassis than later buyers, because the platform is new to them. A flat ratio over-orders in season two and under-orders in season one, which is exactly the wrong way round. The practical correction is to model the installed base rather than the shipment: module demand in any season is a function of how many chassis are in use, not of how many are being shipped that season, and those two curves diverge sharply after the first year.
Lifecycle, Repair and End of Service
Modularity is often presented as a durability argument, and the argument is real but narrower than it is usually stated. A modular product is more repairable only if the failure modes are in the replaceable parts, and on a bag they often are not.
Webbing, buckles and modules are replaceable by design. Panels, anchor rows and harness attachments are not, and those are the parts that fail structurally. A chassis whose anchor row tears has no cheap repair path unless the reinforcement scheme anticipated one, which means designing the anchor area so that a worn field can be replaced rather than requiring the whole panel to be rebuilt.
The end-of-service question is more tractable and more valuable. When a chassis is discontinued, a module designed to the frozen interface still works on the next generation. That is the strongest commercial argument for interface stability, and it is the one that turns an accessory purchase from a bet into a safe decision.
Spare-part availability is the operational half of this. Keeping interface hardware and the highest-demand modules available for a defined period after a chassis leaves the range costs little and is the difference between a platform with a reputation for longevity and one with a reputation for abandonment.
Designing for disassembly is the part usually skipped. A chassis whose webbing field is sewn directly into the load-bearing panel cannot have that field replaced; one in which the field is a separable assembly can. The additional cost is small, the additional seam is a water path that has to be managed, and the benefit is that the single most worn part of the product becomes serviceable rather than terminal.
Recycled-content claims attached to a replacement panel should carry the transaction certificates issued under the scheme maintained by Textile Exchange, so a repair part can be traced to its input stream instead of being vouched for by whoever sold it.
What Would Falsify the Modular Thesis
The modular thesis is a hypothesis about user behaviour, and it is worth stating the conditions under which it fails so that a programme can recognise them early.
| Failure condition | Signal observed | Response available |
|---|---|---|
| Users never reconfigure | Second module purchase rate near zero | Reduce portfolio, sell configured sets |
| Two modules cover all real use | Concentrated sales across the portfolio | Cut the tail, keep the winners |
| Interface causes returns | Detachment or misalignment in return data | Freeze geometry, revise reinforcement |
| Module cost exceeds the value users place on it | Discounting required to clear module stock | Bundle modules into chassis pricing |
| Reconfiguration friction too high | Complaints about attachment effort | Reconsider the engagement mechanism |
The first row is the one that genuinely invalidates the approach. If users configure once and never change, then modularity has delivered a customisation benefit rather than a reconfiguration benefit, and the correct product is a configurable fixed pack sold in variants rather than a platform with a module range.
Everything else in the table is correctable. Interface problems are fixed by freezing geometry and revising reinforcement; portfolio problems are fixed by cutting; friction problems are fixed by changing the engagement mechanism. Only the first row changes the product architecture, and it is measurable within two seasons of launch, which is short enough to act on before the tooling and pattern investment becomes difficult to reverse.
The measurement itself is simple and rarely set up. Record, for each chassis sold, whether a second module was purchased and when. That single ratio separates a reconfiguration platform from a customisation product, and it is the only number that tells a brand whether the architecture it committed to is the one its users are actually using.
For the chassis range built on these rules, see the modular backpack platform, and for the interface geometry itself see the attachment grid engineering notes.
Spec rule: Re-measure any revised interface against the original 38 mm vertical spacing and 50 mm horizontal repeat drawings before release, and record the comparison on lots drawn at AQL 2.5 rather than in a design note.
Frequently asked questions
What actually makes a compartment interchangeable?
A published interface that both the chassis and every module are built to, with toleranced callouts rather than approximate dimensions. Interchangeability is a documentation property before it is a manufacturing one; without the callouts each module renegotiates the geometry.
Why should the interface stay frozen while modules change?
Because its value is a function of its stability. A frozen interface lets modules from earlier seasons mount on later chassis, lets third-party accessories fit without permission, and lets a new module ship without re-testing the platform.
What are the three callouts that define a compatible field?
A 25 mm webbing width, a 38 mm vertical spacing and a 50 mm horizontal repeat, each with a stated tolerance. Those figures are what allow a pouch from another maker to thread the field; without them a grid is decoration.
How many modules should a launch portfolio contain?
Usually fewer than the design team proposes. Each configuration carries MOQ 500 and its own material call-off and setup, so ten modules commit as much setup capacity as a chassis programme ten times over.
How quickly can a module be added after launch?
Plan on 6-10 working days for a straightforward pouch and 12-15 working days once magnetic fittings or moulded corners enter the design. That makes it practical to add a module after demand is demonstrated rather than guessing at launch.
How does modularity change the load path?
Contents transfer through an anchor row at a point with a lever arm rather than into a lining and base. That requires dimensioned reinforcement beyond the stitch line, a stated mass class per row, and a chassis tolerant of asymmetric loading.
Why does a modular chassis need a stiffer back panel?
Because loading becomes asymmetric. One heavy module on one side produces a torsional load through the frame sheet and harness that a symmetrically packed conventional pack never sees.
What is the strongest commercial argument for interface stability?
End-of-service continuity. When a chassis is discontinued, a module built to the frozen interface still works on the next generation, which turns an accessory purchase from a bet into a safe decision.
Is a modular bag more repairable than a conventional one?
Only where the failure is in a replaceable part. Webbing, buckles and modules are replaceable by design; panels, anchor rows and harness attachments are not, and those are the parts that fail structurally.
How should module demand be forecast?
Against chassis sales rather than as independent items, and not as a flat ratio. Early buyers purchase more modules per chassis than later buyers, so a flat ratio under-orders in season one and over-orders in season two.
What production window does a modular release need?
Mass production occupies 35-50 days once materials are in hand, and that window can cover several modules alongside a chassis. The calendar risk sits earlier, in material call-off and interface hardware availability.
When does modularity stop paying for a range?
When users configure once and never change. If second-module purchase rates are near zero, the product has delivered customisation rather than reconfiguration, and configurable fixed variants are the better architecture.
How is interface-driven return data distinguished from product quality?
By the return reason. Detachment, misalignment and stitching at the anchor point to the interface and reinforcement; fabric, coating and zipper complaints point to materials. Separating the two in the return log is what makes the distinction visible.
What is the cost of changing an interface mid-platform?
Every existing module has to be re-checked, retailers re-merchandise, and users with the previous generation find the new pouch does not fit. Where a change is unavoidable, publish a new platform generation rather than altering the existing one quietly.