Home › Field notes › Modular Bags for Outdoor Brands: SKU Architecture and Platforms
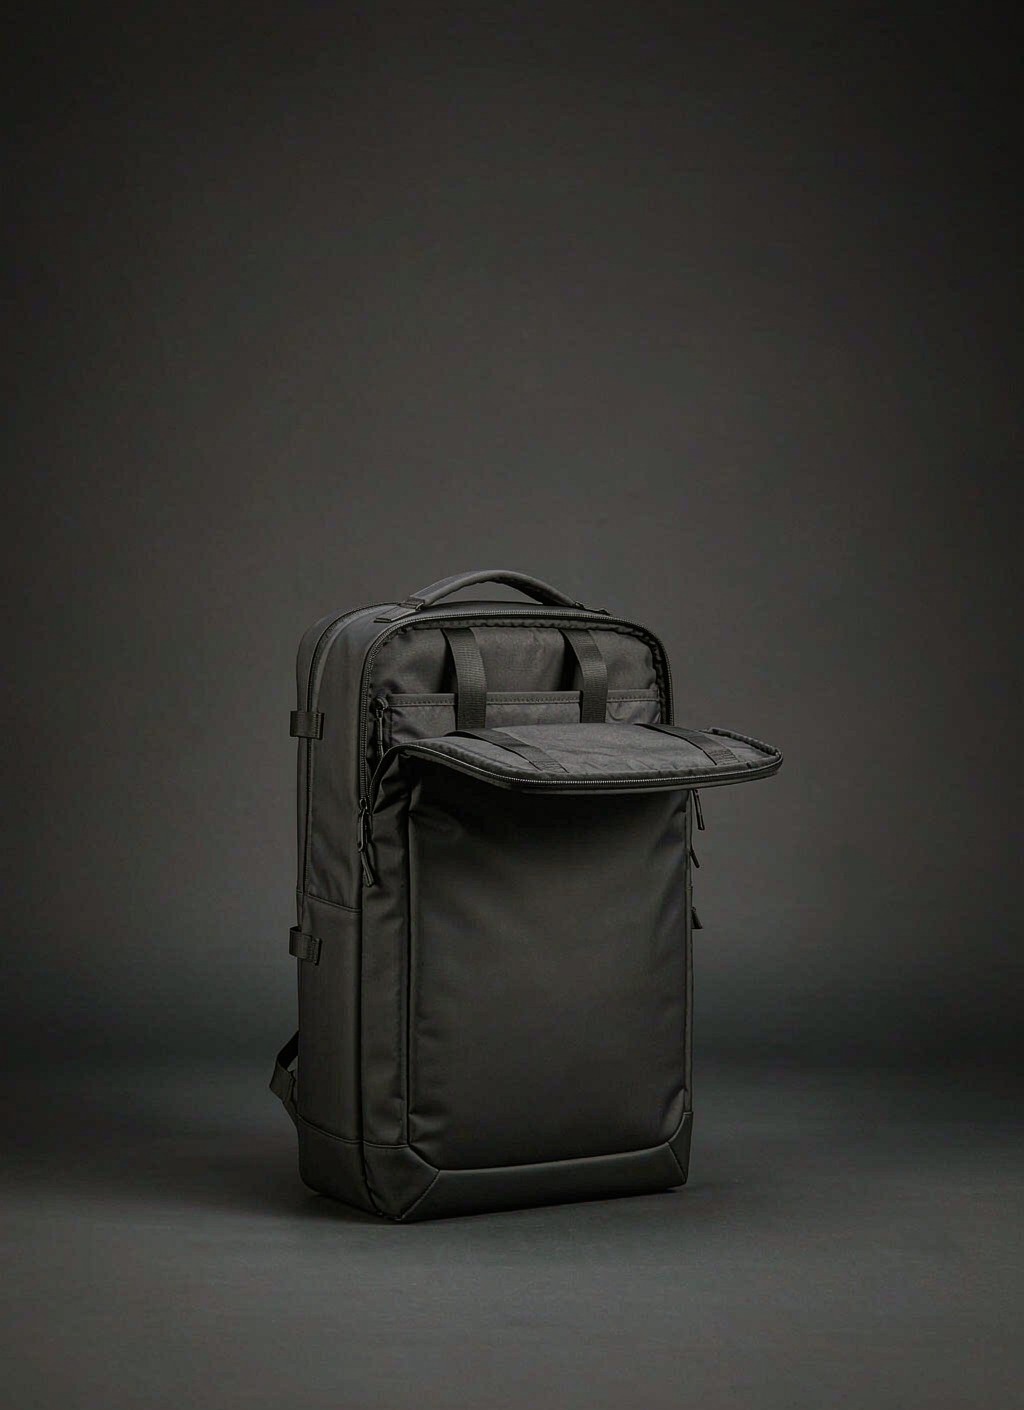
An outdoor brand should design its SKU architecture before it designs its next bag, because the architecture decides the tooling spend and the inventory risk for several seasons. The modular answer is a shared carrier with a library of modules: one chassis carries the interface, the modules carry the differentiation, and a range of ten configurations can sit on two committed shells. Interface standardisation is what makes this durable — 25 mm webbing on 38 mm rows repeating every 50 mm — because a module released in year three still fits a shell released in year one. Minimum order quantity is 500 units per specification and tooling runs USD 300–2,500. The sections below cover each layer of that decision.
Capacity ladders, colourway splits, margin structure and a seasonal calendar distinguishing carry-over from new development complete the architecture. Backwards compatibility, module attach rate and the annual architecture review are treated as commitments rather than preferences.
SKU count is the decision that decides everything else
Outdoor ranges accumulate SKUs the way gardens accumulate plants: each addition is justified in isolation, and nobody removes anything. A range that started with six bags is at twenty-four within four seasons, and the working capital, the forecasting burden and the markdown exposure have all grown faster than the revenue behind them.
The arithmetic of proliferation is unforgiving. Twenty-four SKUs at 500 units each is 12,000 units of committed inventory before any of them has sold. The same twenty-four configurations built on two shared shells is 1,000 units of shell inventory plus a much smaller and cheaper module inventory, and the module inventory turns faster because modules are cheaper and reorder more quickly.
| Cost line | Twenty-four standalone bags | Two shells plus a module library | Where the difference comes from |
|---|---|---|---|
| Tooling and setup | Twenty-four sets of patterns, dies and markings | Two shell toolings plus module patterns | USD 300–2,500 per setup item, repeated per standalone bag |
| Committed inventory at opening | About 12,000 units | About 1,000 shells plus modules | The floor applies per specification, not per configuration |
| Forecast error exposure | Twenty-four independent forecasts | Two shell forecasts plus module demand | Modules can be reallocated between shells |
| Test evidence required | Each bag needs its own commission | Shell tested once; modules tested for interface | A shared carrier carries shared evidence |
| Markdown exposure at end of season | Twenty-four slow lines | Modules are cheap to discount; shells carry over | Carry-over shells with new modules |
| Dealer line-sheet complexity | Twenty-four lines to explain | One platform story plus a module matrix | Simpler sell-in, clearer merchandising |
The table understates the advantage in one respect and overstates it in another. It understates the flexibility: a module can be released mid-season without touching shell production, which turns a trend response from a two-season project into a single run. It overstates the saving in one respect, because a module library still has its own tooling, its own inventory and its own forecasts, and a library that grows without discipline reproduces the original problem at a smaller scale.
The governing rule is that differentiation should be pushed as far down the cost curve as possible. Colour, module and marking are cheap to vary; shell geometry is expensive. A range that varies at the cheap end and standardises at the expensive end is structurally more profitable than one that does the opposite.
Selection rule: Cap the number of active shells first and let colourway, trim and marking carry the visible variation, because those three vary cheaply while shell geometry does not, and every new colour still has to clear the 500-unit floor to be economical.
The shared carrier: what stays fixed and what varies
A platform needs a written statement of what is fixed, because without one the fixed elements drift and the platform silently stops being a platform. The fixed list normally contains the interface geometry, the harness attachment, the base construction and the marking placement. Everything else is variable.
Interface geometry is the item that must never move. Webbing at 25 mm, rows at 38 mm vertical spacing, columns repeating every 50 mm, held to a stated tolerance across a stated cumulative distance. That geometry is what makes every module fit every shell, and a drift of a couple of millimetres is enough to make a module mount stiffly, which users read as a defect even though nothing is broken.
Tolerance needs to be specified on the repeat and on the cumulative distance, not on individual rows. Individual rows can each be within tolerance and still accumulate into a field that will not accept a module at the bottom. Specify the cumulative figure across ten rows and check it with a gauge at inspection.
The variable list is where the range lives: capacity, colourway, lining specification, module set, hardware grade and marking. Those are the dimensions a brand can change season to season without invalidating anything the customer already owns, and that is the promise worth making in the marketing.
Backwards compatibility should be treated as a public commitment rather than an internal preference. If a brand tells customers that modules fit across seasons, it has to hold the geometry across seasons, which means the interface specification belongs in the brand's own product standards rather than in a supplier's tech pack alone.
Verdict: Write the fixed list into the brand's own product standards rather than into a supplier document alone, including the 25 mm grid pitch and its tolerance, because a platform whose fixed elements drift silently stops being a platform.
Sizing the module library
The library is the part of a modular range that most often gets sized wrongly. Too small and the platform offers no differentiation, so the range looks like two bags. Too large and the library reproduces the SKU problem it was meant to solve, with the added burden that every module has to be tested against the interface.
| Library size | Inventory implication | Interface testing load | Range story supported |
|---|---|---|---|
| Three modules | Minimal; one run each at the 500-unit floor | Three interface commissions | A shell with options; weak differentiation |
| Five to six modules | About 3,000 units across the library | Five or six commissions, evidence largely shared | Clear categories: hydration, camera, tools, clothing, first aid |
| Nine to twelve modules | Substantial; forecast burden returns | Full commission per module plus compatibility matrix | Strong ecosystem; needs genuine volume behind it |
| Above twelve | The original proliferation problem returns | Matrix testing grows quadratically | Only defensible with an accessory business of its own |
Five or six is the right target for most brands. It is enough to tell a clear category story — hydration, camera, tools, clothing, personal organisation and first aid — and small enough that each module has a real reason to exist. Below that, the modular claim is thin; above it, the library needs its own merchandising and forecasting discipline.
Every module should have to justify its place annually. A simple review measuring units sold, attached-to-sales ratio and margin contribution, run once a season, keeps the library from drifting upwards. Kill the bottom module each season unless it is strategically necessary, because a module that exists only in the catalogue is a cost without a purpose.
Track the attach rate: modules sold divided by shells sold. It is the single best indicator of whether the platform story is landing with customers, and it also tells the brand how much inventory to hold. An attach rate near 1.0 means customers buy one module; near 2.5 means the ecosystem is working and the library can support more depth.
Capacity ladders and how many sizes a range needs
Outdoor ranges tend to offer more capacities than the market needs. Three sizes is usually right: a day capacity around 20 to 25 litres, a weekend or overnight capacity around 32 to 40 litres, and a travel or expedition capacity above 50 litres. Each has a distinct use and a distinct customer, and the gaps between them are wide enough that a customer can self-select without a fitting guide.
A fourth size rarely earns its place. It sits between two existing capacities, competes with both, and inherits the forecasting burden of a separate specification. Where a retailer insists on exclusivity, an exclusive colourway is a cheaper concession than an exclusive size, because it shares the pattern, the tooling and the test evidence.
The ladder should also be honest about what modular does to capacity. A shell rated at 25 litres plus three external modules has a usable capacity that is larger than 25 litres but behaves differently, because the external mass is further from the body. State the shell capacity and the module capacity separately and do not add them into a single headline number, which is a claim a customer will test.
Fit is the other half of the capacity decision and the harder one to specify. A harness that fits a 25-litre day load will not carry a 40-litre expedition load comfortably, so the harness specification differs across the ladder even where the shell interface is shared. Standardise the interface, not the harness.
One size-related decision deserves explicit attention: torso length. Offering two torso lengths on the larger capacities is more valuable than offering an extra capacity, because a badly fitting heavy pack generates returns and negative reviews that no feature set compensates for.
Bottom line: Offer three capacities rather than five and spend the difference on two torso lengths in the larger sizes, since every additional size has to justify its own 500-unit run and a badly fitting heavy pack returns faster than any feature sells it.
Colourway economics under the 500-unit floor
Colour is the cheapest differentiation available and the most dangerous. It is cheap because a colourway shares the pattern, the tooling and most of the test evidence. It is dangerous because every colourway is a separate specification at the 500-unit floor, and demand across colourways is never even.
The standard pattern is a 60/30/10 split across three colourways, and it holds often enough to plan on: the core colour takes around 60 % of units, the second around 30 %, and the accent around 10 %. A brand opening at 1,500 shells might therefore commit 900, 450 and 150 units. The accent colourway is the one that will be discounted if the split is wrong.
Minimums interact with this awkwardly. At 500 units per colourway, a three-colourway opening is a 1,500-unit commitment. A brand that cannot support that should open with one core colourway and one accent, and add the third in the second season against real data rather than opening with three against a forecast.
Continuity matters more in outdoor than in most categories, because customers and retailers build ranges around a colour that is expected to persist. A core colourway should be committed for at least three seasons, and any change announced a season ahead. Rotating accent colourways is fine; rotating the core is not.
Dye-lot control is the technical discipline behind all of this. A retained physical standard from the approved lot, a stated tolerance against it, and a dye-lot declaration from the fabric supplier are what keep the core colour recognisable across three seasons of production. Without them, the core colour drifts and the range looks inconsistent on a dealer's wall.
Takeaway: Hold dye-lot references and a shade band card for the core colour and limit each season's new shades to what one order can support, because colour is cheap to vary and expensive to spread thin.
Price ladder, margin and where the platform earns its money
A platform changes the margin structure of a range, and not always in the direction brand owners expect. Shell margins are usually lower than the previous standalone range, because the shared development cost has to be recovered across fewer distinct products. Module margins are usually higher, because modules are cheap to make and are bought by customers who have already committed to the platform.
The commercial consequence is that the platform earns its money on attachment rather than on the first sale. A brand should plan the shell price to be competitive and the module margin to carry the range, then measure the attach rate as the primary commercial indicator rather than the shell sell-through alone.
Bundles are where this is executed. A shell plus one module at a modest premium over the shell alone raises the average order value and introduces the customer to the ecosystem; a shell plus three modules at a larger discount builds the attach rate faster at the cost of margin. Which to lead with depends on whether the brand is optimising for this season's revenue or for the installed base.
Accessory revenue has a second characteristic worth planning for: it is less seasonal than shell sales. Modules are bought as replacements, as gifts and as additions long after the shell purchase, which smooths the revenue curve and reduces dependence on the seasonal launch. This is a genuine financial benefit of the architecture, and it belongs in the business case.
Set the price ladder so that a fully configured shell costs more than a competing standalone bag but clearly delivers more. A configuration that costs 30 % more and offers four use cases is defensible; one that costs 60 % more is not, however good the engineering. The ladder should be designed against the competitor set rather than against internal cost.
Judgement: Design the price ladder against the competitor set rather than against internal cost alone, remembering that modules are what lift programme margin above the chassis price rather than anything the shell does.
Test evidence across a platform rather than per SKU
One of the largest hidden savings in a platform architecture is in testing. A standalone range commissions a full set of tests per bag; a shared carrier commissions the shell once and then tests each module for its interface behaviour. The saving is substantial and it compounds every season the shell carries over.
The shell commission covers the fabric and construction properties: tensile strength under ASTM D5034, abrasion under ASTM D3884 or ISO 12947, coating adhesion under ASTM D751, hydrostatic head under AATCC 127, colour transfer under AATCC 8 and hardware corrosion under ASTM B117. That commission stays valid while the shell is unchanged, and a colourway change does not invalidate it.
The module commission is different and smaller. It covers the interface: pull-out and peel behaviour at the anchor, cycling of the closure, and dimensional compatibility with the interface gauge. Because the shell geometry is shared, the module test is a compatibility and durability question rather than a full material evaluation, and it costs a fraction of a standalone bag commission.
Keep the evidence organised as a platform file rather than as per-SKU folders. A file indexed by component, with the test method, the date, the lot reference and the result, lets a brand answer a retailer's question in an afternoon and makes a carry-over decision evidence-based rather than a matter of opinion.
Re-test on a defined trigger rather than on a schedule. Change of fabric supplier, change of coating, change of hardware supplier or a change to the interface geometry should each trigger a re-commission. An unchanged shell in a new colourway should not, and a brand that re-tests unnecessarily is spending margin for no informational gain.
Seasonal calendar: carry-over against new development
Outdoor ranges run on a seasonal calendar that is longer than most brands plan for, and a platform architecture changes which parts of it are critical. The new-development path is long; the carry-over path is short; and modules are shorter still. Distinguishing the three is what makes the calendar manageable.
A new shell is the long path. A reference piece takes 6–10 working days, 12–15 where the construction is complex; the first production run takes 35–50 days from approval; ocean transit takes 25–35 days. Add dealer line-sheet preparation and a sell-in period before that, and a new shell developed for an autumn season is being specified in the preceding spring.
Carry-over is far shorter. A shell already in production with fabric and hardware reserved can be re-run in roughly the production window alone, which means a re-order decision can be made much later against real sell-through data. This is the single biggest planning advantage of a platform: the expensive item becomes the flexible one.
Modules are the shortest path of all and the most useful. A new module can be developed and produced inside a single season, which means a trend response or a retailer request can be met without the multi-season lead time of a new bag. Brands that exploit this treat the module library as their fast-response capability.
Plan the season as a mix rather than as a list. A typical healthy season is one carry-over shell, one new module, and a new colourway: low risk, low development cost, and a genuine reason for a retailer to revisit the range. A season of all-new shells is a bet, and outdoor brands that place it repeatedly eventually lose one.
Capacity should be declared on a rolling basis. Our production side works 7 production lines with 137 people and 149 machines across a 4,950 m² SGS-verified production floor at 200,000 units per month, and a brand that declares two seasons of shell volume gets fabric and hardware reserved against it, which is what turns carry-over from a hope into a booking.
Writing the platform specification so it survives staff changes
A platform is a long-lived asset and it will outlast the people who specified it. The specification therefore has to be written for a reader who was not there, which means stating assumptions, decisions and the reasons behind them rather than only the dimensions.
Four documents make up the file. An interface standard, with the geometry, the tolerances and the gauge method. A component register, listing every shell, module and hardware item with its supplier, its material and its approval reference. A test file, indexed by component and method. And a change log, recording every deviation with its date and its justification.
The change log is the one most often missing and the one that matters most after two years. A deviation made for a cost reason in one season, and forgotten, becomes a compatibility problem three seasons later when a new module is designed against the drawing rather than against the shipped product. Record every deviation, however small.
State the compatibility promise publicly and honour it. If the brand tells customers that modules fit across the range, then the interface standard is a commercial commitment and should be treated as one in every change review. Breaking it silently is the fastest way to convert a platform advantage into a complaint.
Finally, review the architecture annually rather than continuously. One scheduled review, with the attach rate, the module ranking, the shell forecast accuracy and the test file in front of the team, produces better decisions than a series of incremental adjustments made under seasonal pressure.
Spec rule: Keep one living document holding the fixed list, the tolerance set covering 25 mm tape width, 38 mm vertical spacing and 50 mm horizontal repeat, the module ranking, the test file and the forecast, reviewed each season so staff changes do not quietly rewrite the platform.
Frequently asked questions
How many SKUs should an outdoor range carry?
Far fewer than most do. Twenty-four configurations on two shared shells is workable; twenty-four standalone bags means about 12,000 units of committed inventory at the 500-unit floor, twenty-four forecasts and twenty-four test commissions.
What must stay fixed on a modular platform?
The interface geometry above all: 25 mm webbing on 38 mm rows repeating every 50 mm, held to a stated tolerance. Also the harness attachment, the base construction and the marking placement. Everything else can vary season to season.
How should interface tolerance be specified?
On the repeat and on the cumulative distance across ten rows, not on individual rows. Rows can each be within tolerance and still accumulate into a field that will not accept a module at the bottom. Verify with a gauge at inspection.
How many modules should a library contain?
Five or six for most brands, enough to cover hydration, camera, tools, clothing, personal organisation and first aid. Below three the modular claim is thin; above twelve the library reproduces the SKU problem at a smaller scale.
What is an attach rate and why does it matter?
Modules sold divided by shells sold. Near 1.0 means one module per customer; near 2.5 means the ecosystem is working and the library can support more depth. It is the best single indicator of whether the platform story is landing.
How many capacity sizes does a range need?
Three: roughly 20 to 25 litres, 32 to 40 litres, and above 50 litres. A fourth usually competes with both neighbours. Two torso lengths on the larger capacities add more value than an extra capacity.
How should colourways be split across a first order?
Plan on 60/30/10 across three colourways. At 500 units per colourway that is a 1,500-unit opening commitment, so a brand that cannot support it should open with two colourways and add the third against real data.
How long should a core colourway be committed?
At least three seasons, with any change announced a season ahead. Accent colourways can rotate freely; rotating the core makes the range look inconsistent on a dealer wall and breaks retailer range planning.
How is dye-lot consistency maintained across seasons?
Hold a retained physical standard from the approved lot, state a tolerance against it, and require a dye-lot declaration from the fabric supplier. Without those three the core colour drifts and customers notice.
Where does a platform earn its margin?
On attachment, not on the first sale. Shell margins are usually lower than a standalone range because development is shared; module margins are higher and recur. Plan the shell price competitively and let the module margin carry the range.
How much testing does a platform save?
A great deal. The shell commission covers ASTM D5034, ASTM D3884 or ISO 12947, ASTM D751, AATCC 127, AATCC 8 and ASTM B117 once. Each module then needs only interface testing for pull-out, peel, closure cycling and gauge compatibility.
When should a shell be re-tested?
On a trigger, not a schedule: a change of fabric supplier, coating, hardware supplier or interface geometry. A new colourway on an unchanged shell does not require a re-commission, and testing unnecessarily spends margin for no information.
How long before the season must a new shell be specified?
A full season ahead. A reference piece takes 6–10 working days, 12–15 where complex; the run takes 35–50 days; ocean transit takes 25–35 days; and dealer sell-in sits before all of that.
What is the advantage of carry-over shells?
Speed of decision. With fabric and hardware reserved, a shell can be re-run in roughly the production window alone, so the reorder is made against real sell-through data rather than a forecast made a year earlier.
What documents make up a platform file?
Four: an interface standard with tolerances and the gauge method, a component register with suppliers and approvals, a test file indexed by component and method, and a change log recording every deviation and its justification.
Why is the change log so important?
Because a small cost-driven deviation, forgotten, becomes a compatibility problem when a new module is designed against the drawing rather than the shipped product. Record every deviation, however minor, and review the architecture annually.