Home › Field notes › Modular Bags for Sports Teams and Clubs: Kit Room Specification
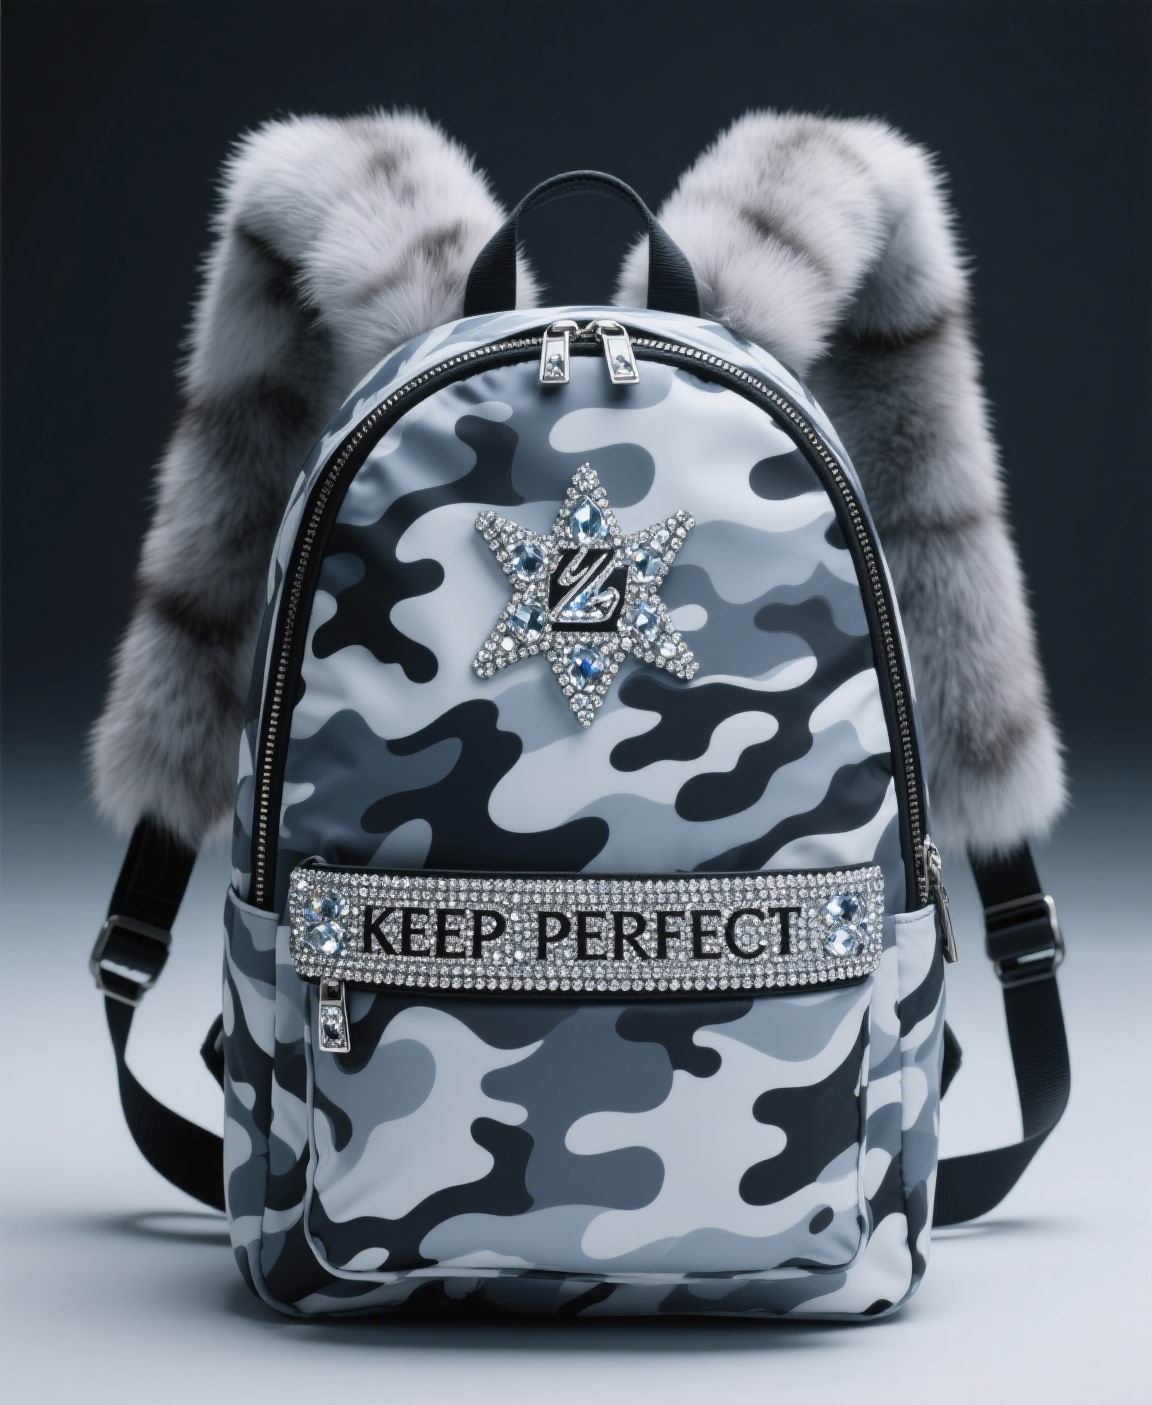
Modular bags suit sports clubs because the squad list turns over faster than the equipment does, and a platform built around interchangeable attachments lets the club reissue kit without redeveloping the carrier every registration window. Practically, that means specifying one chassis, two or three size codes and a set of task pouches, then letting attachments carry the identity that printed names used to carry. Volume floors still apply: MOQ 500 per module reference is the number that governs how many distinct attachment types survive costing, and it interacts directly with size splits across a roster. Decoration durability then decides whether the club reorders, measured through repeated domestic laundering rather than appearance on day one. This guide sets out the roster arithmetic, the construction responses required by a damp kit room, the wash and rub evidence worth demanding, and the calendar that gets the carrier delivered before pre-season rather than after it.
What a club actually buys: one carrier, several jobs
A team kit manager rarely wants one bag; they want one funding line that covers three or four different jobs. The same person responsible for the match-day holdall is often responsible for the training-ground wash load, the away-trip duffel and occasionally the coach's documentation folder. A single-purpose product forces them to buy three articles from three budgets. A shared platform funded once, with attachments assigned by role, usually wins the internal argument on grounds of simple accounting.
That buying logic shapes the specification in concrete ways. The chassis must be size-tolerant enough to serve a seventeen-year-old and a staff member, which pushes toward adjustable harness geometry rather than sculpted shoulder foams cut for one torso length. It must accept hard, dirty contents without complaint: boots, a wet towel, a drink bottle and a spare shirt all live in the same compartment for at least part of every week. And it must clean, because a junior squad will put things in it that no product designer anticipated.
Attachments then differentiate the roles rather than different bags doing so. A ventilated boot compartment suite works for the match-day build; a wet-goods pouch handles the post-training wash run; a document sleeve turns the same shell into something acceptable at a club registration meeting. The commercial advantage for a brand selling into this channel is that each of those roles is a separate reorder line attached to a platform the club already trusts, which is a far cheaper sale than convincing the club to replace its whole carrier.
For our production team the practical instruction is straightforward: hold the chassis rigid and let modules flex. Chassis changes invalidate every module already in the field, while module changes only affect the new reference. That asymmetry is why we strongly resist requests to alter body dimensions mid-season, even when the requested change appears trivial on a drawing.
Verdict: Buy one adjustable chassis across two or three size codes and let attachments carry role identity, because squad turnover outpaces equipment life by roughly two registration windows every year.
Roster volatility and why printing names is not a strategy
The most expensive mistake in this channel is treating identity as a print job. Embroidery or a heat-applied number at volume looks economical until the club re-registers in January and eight squad members either left or moved numbers. Suddenly the entire carry stock carries names of people nobody recognises, and the club either reissues (expensive) or hands new players anonymous bags (undermining the sponsor visibility that justified the spend).
The alternative is to move identity onto the detachable layer. A permanent chassis carries only the club crest and the sponsor lockup; the individual belongs to a module or a removable panel that can be swapped for a small fraction of replacement cost. Junior academies particularly benefit, because their registration churn is highest and their budgets are thinnest.
There are three workable identity-bearing layers. A printed or embroidered name panel on a detachable pouch, which is cheapest to reissue but only visible when the pouch is attached. A hook-and-loop-backed identifier panel in a protected position on the chassis, which survives removal but accumulates grit in the loop field over a season. Or a numbered tag system using hardware-mounted plates, which reissues cheapest of all but adds a small part count to manage in the kit room.
Whichever route is chosen, specify the replacement pathway at the same time as the original. Clubs will ask "what happens when someone leaves" and the answer should already exist in the range plan, with a reference code, a unit cost and a lead time attached. That answer is often the deciding factor in a competitive tender.
Bottom line: Keep the crest and sponsor lockup on the chassis and move player identity onto a swappable panel, since reissuing a printed shell costs several times the price of a replacement module at MOQ 500 per reference.
Decoration routes and the wash evidence behind each
Clubs launder kit bags more aggressively than any other customer group, and often at higher temperatures than the care label permits. Decoration selection therefore has to be made against evidence from repeated domestic laundering and subsequent visual grading, not against first-day appearance. A route that looks superb on a sales sample and cracks at cycle fifteen will generate complaints for the rest of the season.
| Route | Identifiers per unit | Behaviour through repeated laundering | Cost driver | Best fit |
|---|---|---|---|---|
| Embroidery | Issued as fixed unit | Stable; puckering managed through backing choice | Stitch count and colour changes | Club crest and sponsor lockup |
| Heat-applied transfer | Variable per unit at low incremental cost | Edge lift risk near panel seams after repeated cycles | Film area and press time | Playing numbers if replacement is planned |
| Woven badge | Fixed unit | Very stable; edges must be bound or overlocked | Loom setup and minimum loom quantity | Heritage crests and founding year |
| Printed panel | Arbitrary per unit | Grade depends on ink system and cure control | Registration accuracy across colours | Sponsor rotation and short-run events |
| Hardware-mounted plate | Swapped by the club | Unaffected by laundering | Component count and spares logistics | Squad numbers with high churn |
Two of these routes deserve a warning. Heat-applied transfers are the cheapest way to personalise, and also the most common source of mid-season complaints, because adhesion depends on consistent press temperature and dwell that small decoration subcontractors do not always document. If you choose it, require a wash trial result before bulk rather than accepting a supplier's generic claim. Printed panels vary enormously by ink system; a water-based system behaves very differently to a plastisol deposit through the same machine.
The colour-fastness question is separate and often overlooked. Dark club colours rub against light kit during transport, and AATCC 8 crocking grades are the right starting metric, with attention to wet rubbing in particular. Repeated laundering evidence under ISO 6330 then covers appearance retention. Write both into the tech pack with numeric grades, because "colourfast" means nothing measurable.
Takeaway: Require wash evidence to ISO 6330 with a stated cycle count plus rub colour fastness to AATCC 8 recorded dry and wet before any decoration route is approved for bulk.
Kit-room storage: damp, stacked and never fully dry
Ask any kit manager where the damage happens and they will point at the pitch. They are usually wrong. The majority of structural failures in club equipment originate from how it is stored: stacked wet, in an unheated room, for eleven months a year. Understanding that environment changes several specification decisions in ways that field-testing alone never would.
Start with linings. A coated interior that traps moisture is the single most reliable way to grow odour and mildew staining in a shared storage room. A breathable, wipe-clean lining with a genuinely open structure performs better over a season even though it looks less premium on the sales floor. Where waterproof performance is genuinely required, isolate that requirement in a removable wet pouch rather than coating the whole interior.
| Kit-room condition | Dominant damage mechanism | Specification response | Evidence to request |
|---|---|---|---|
| Stacked wet under load | Coating hydrolysis and blocked seam stress | Breathable lining, reinforced base, drainage path | Accelerated ageing followed by coating adhesion check |
| Cold unheated room | Embrittlement of face coating | Coating chemistry rated for low-temperature flex | Low-temperature bend assessment before visual grading |
| Repeated machine washing | Seam tape lift and thread shrinkage movement | Preshrunk components and matched shrinkage rates | Dimensional change data after ISO 6330 cycles |
| Contact with studs and buckles | Abrasion and puncture at the base panel | Higher denier base, bound internal seams | Abrasion cycles reported by panel position |
| Disinfectant spray routines | Chemical attack on prints and transfers | Chemically resistant decoration system | Spot-exposure trial documented with photographs |
The final row catches many programmes unawares. Hygiene protocols introduced across amateur sport in recent years mean hard surfaces get sprayed regularly, and some disinfectant chemistries will haze or lift printed decoration within weeks. It is a cheap question to ask during development and a ruinous discovery in February.
Judgement: Specify a breathable wipe-clean lining with a drainage path instead of a fully coated interior, because eleven months stacked damp in an unheated room destroys more kit than any pitch surface manages.
Match day, training night and travel day: three duty profiles
The same carrier serves three jobs with remarkably different loads. Treating them as one duty profile produces a chassis that compromises everywhere rather than performing anywhere. Separating them clarifies which compromises are actually acceptable.
Match day is a low-volume, high-delicacy profile. Kit is usually clean, contents are predictable, and appearance matters because sponsors photograph it. The requirement here is organisation: separated boot storage, a valuables position that zips closed, and a flat external document position for team sheets. Total capacity demand is moderate, typically well below what the same club expects on a travel day.
Training night is high-volume and filthy. Contents arrive wet, muddy and unsegregated, and nothing needs to look presentable. Capacity demand peaks here, along with the requirement that every surface survive hosing down. This profile, not match day, drives the lining specification and the drainage requirement.
Travel day is about cabin compliance and security. The carrier has to meet whatever dimensional rule the airline applies, contents have to survive being opened at a checkpoint, and the whole thing has to be carried for longer distances than any of the other profiles require. Checking against IATA guidance during development prevents an embarrassing rejection at a departure gate with twenty players waiting.
Specifying three profiles does not mean building three chassis. It means confirming that one chassis plus the appropriate attachment set covers all three acceptably, and identifying explicitly where a compromise was chosen. Written-down compromises are defensible; accidental ones become complaints.
Artificial turf, boot studs and mud: the failure set clubs report
Artificial surfaces have changed the failure profile of sports equipment significantly. Rubber crumb infill is abrasive, gets everywhere and works into zip tapes and binding edges with impressive persistence. Boots with aggressive stud patterns puncture base panels that were perfectly adequate on grass. Together these two factors explain most of the premature failures clubs attribute to "poor quality".
Zips are the first casualty. Crumb ingress into the coil jams sliders and eventually wears the tape. The two workable responses are covered zip garages on the base-facing runs and heavier-gauge coil selection, with a specified dust-ingress trial rather than just a cycle count. A zip that survives twenty thousand clean cycles tells you little about six months on a 3G surface.
Base panels are the second casualty. Specify higher denier fabric on the panel likely to meet studs, bind rather than turn internal seams so that a puncture has nowhere to propagate, and consider a sacrificial wear strip. Weigh these against carried comfort, but remember that a holed base at week nine destroys more brand equity than an extra 40 grams ever will.
Binding edges and webbing absorb grit in the third failure mode. Because the same webbing standard serves the attachment system, this matters structurally: a field contaminated with crumb stiffens, threading force rises, and modules stop seating properly. Where a club uses a platform with 25 mm webbing attachment rows, arrange periodic cleaning guidance in the care instructions and test threading after contamination rather than only when new.
Spec rule: Cover every ground-facing zip run, choose a heavier-gauge coil at those positions, and add a dust-ingress trial to the specification rather than relying on a clean twenty-thousand-cycle figure alone.
Roster arithmetic: how one order splits across sizes and colours
Club orders are almost never one reference. A single senior squad might want two size codes, an academy wants three, and coaching staff want a fourth treatment. Meanwhile every module sits against MOQ 500 if placed as a standalone reference. Reconciling those two facts is the core commercial task of this channel.
The workable approach is to pool the chassis. Because a chassis is one pattern across size codes, size splits generally aggregate against the platform rather than individually, which is why a structured platform has an advantage over a fragmented one. Colourways are harder: a colourway is effectively a separate commit for the cutting room, so colour should be the variable you hold to one unless the club can fund the split.
| Variant axis | Typical club request | Quantity consequence | Guidance |
|---|---|---|---|
| Size code | Two to four codes | Aggregates against the platform pattern | Approve freely; cost impact is modest |
| Chassis colour | Home and away options | Each colourway consumes separate cutting capacity | Approve only against confirmed volume |
| Attachment type | Three to six types | Each reference carries MOQ 500 | Launch with two, expand on reorder |
| Personal decoration | Per player | Per-unit handling and spares provisioning | Put identity on a swappable layer |
| Sponsor artwork | Seasonal rotation | Screen or plate setup per artwork | Budget USD 300-2,500 per setup element |
The recurring error is launching with the full catalogue of attachments on day one. Six attach concepts sounds generous, and it converts immediately into six reference commitments that individual sales have not earned. Launch with two, sell those, and add a third on the reorder. Given that development samples run USD 50-150 each and are refundable against production, incremental development is inexpensive; unsold committed inventory is not.
Working the calendar back from the first fixture
Delivery failures in this channel are calendar failures, almost never production failures. A club orders in May because a committee meets in May, expects delivery in July for pre-season, and nobody has reverse-engineered whether that is physically possible. It often is not, and the resulting compromise damages the relationship for years.
Start from the date the kit must physically be in the club's hands, then subtract inward inland delivery, then transit. Sea freight 25-35 days is the planning assumption; air 5-8 days exists for genuine emergencies and blows the budget for routine ones. Subtract inspection and release of the balance under T/T 30/70, then mass production 35-50 days, then development: 6-10 working days for a straightforward pouch concept and 12-15 when moulded shells, structured foam or complex harness assemblies are involved.
Add a buffer for the decision loop, because committee decisions take longer than any production step. In practice a club committee needs two meetings to approve artwork, and those meetings are usually monthly. Model that explicitly rather than assuming a prompt reply, and place the approval gate where it belongs: before tooling is committed, not after.
Finally, plan the second year during the first. The lowest-cost reorder any brand can win is one against a platform the club already owns, where the new business is simply an additional attachment reference. Record which attachment interfaces shipped in year one, keep the geometry frozen, and the year-two conversation becomes a catalogue discussion rather than a seven-month development project.
Selection rule: Set the booking date by working backwards from the first fixture through mass production 35-50 days and sea freight 25-35 days, then add two committee meetings before any tooling spend is committed.
Frequently asked questions
What is the minimum order for a club modular bag programme?
Each attachment type is quoted against MOQ 500 as a standalone reference, while size codes on one chassis generally aggregate against the shared pattern. In practice a senior squad plus academy can clear that comfortably; a single small team often cannot. The remedy is to pool across age groups and staff rather than reducing the platform quality to hit a lower quantity.
Should clubs put squad numbers on the chassis or on a detachable layer?
Put the crest and sponsor on the chassis and move player identity to a swappable layer. Registration churn in youth sport runs high, and reissuing a printed or embroidered shell costs several times more than replacing a numbered panel or plate. Plan the replacement pathway during development, with a reference code and unit cost attached.
How many washing cycles should a club kit bag survive?
Set the target against how clubs actually behave, which is far more aggressive than any care label. Two seasons of weekly washes suggests a target in the region of fifty domestic cycles, verified by ISO 6330 with visual grading, plus rub colour fastness under AATCC 8 recorded both dry and wet. Require the cycle count in the specification, not an adjective.
Which decoration method resists disinfectant spraying best?
Embroidered crests and hardware-mounted plates are essentially unaffected by spray routines. Heat-applied transfers and some print systems haze or lift under repeated chemical exposure. Whichever route you select, run a documented spot-exposure trial during development, because several hygiene chemistries used in amateur sport attack plastisol deposits within weeks.
Why do zips fail early on artificial pitches?
Rubber crumb infill works into the coil and tape, raising slider friction until the tape wears through. Clean-cycle testing understates the problem badly. Specify covered zip garages on any run facing the ground, choose heavier-gauge coils for those positions, and add a dust-ingress trial rather than relying on a bare twenty-thousand-cycle figure.
Can one chassis really serve both the academy and the senior squad?
Yes, provided the harness is adjustable rather than sculpted. Size-tolerant shoulder geometry with sufficient adjustment travel covers a wide torso range, whereas foam cut for one length suits nobody at the extremes. Confirm fit across the smallest and largest expected users during development rather than testing only the median size.
How early must a pre-season delivery be ordered?
Work backwards from the date kit must physically arrive. Mass production 35-50 days plus sea freight 25-35 days plus inspection and payment release under T/T 30/70 already exceeds ninety days, and that excludes development at 6-10 working days, or 12-15 with moulded or padded construction. Add committee approval loops on top, and the realistic lead from art approval is close to five months.
What should we do about odour in a shared kit room?
Design the interior to dry. A breathable, wipe-clean lining with an open structure outperforms a fully coated one even though it photographs less expensively, and a drainage path in the wet pouch stops moisture pooling at the base. Where water resistance is genuinely needed, confine it to a removable pouch and leave the main body able to breathe.
Are loyalty programmes better served by more colours or more attachments?
More attachments, consistently. Colour multiplies cutting-room complexity and inventory risk without changing what the user can do, whereas an additional pouch adds a capability and a reorder line against a platform already trusted. Track it empirically: additional colourways typically redistribute existing demand, while new attachment types frequently open a purchase that would not otherwise occur.
What causes the recurring complaints about print cracking on club kit?
Usually a deposit that is too thick for the fabric movement, or insufficient cure control at a decoration subcontractor. Both present identically as cracking after repeated laundering. Require evidence from a documented wash trial rather than a generic durability claim, and specify thinner transfers on panels that flex sharply in use.
Should we use air freight to rescue a late pre-season delivery?
Air 5-8 days rescues genuine emergencies and quietly destroys programme economics when used routinely. Compare the freight premium against a phased handover: shipping the chassis and first attachments by sea freight 25-35 days and following with later modules often arrives close in usefulness at a fraction of the cost. Reserve air freight for situations where absence would damage the relationship.
How do we keep modules compatible across successive seasons?
Freeze the interface geometry and resist small body changes. Once 25 mm webbing, 38 mm vertical spacing and 50 mm horizontal repeat are locked with stated tolerances, later attachments will fit earlier chassis. Changing the pattern to add one row invalidates everything already in the field and should be deferred to a clear season boundary with written notice to existing clubs.
What capacity is available if a federation-level programme scales quickly?
Up to 200,000 units per month is available from our SGS-verified production base, across 7 production lines with 149 machines and 137 people on a 4,950 m² floor. Capacity is rarely the constraint; changeovers are. Keep colourways tight and module references few, and volume scales cleanly; spread the same units across many variants and the schedule stretches regardless of headline output.