Home › Field notes › Modular Bag Wholesale: Bulk Buying Terms for Retail Chains
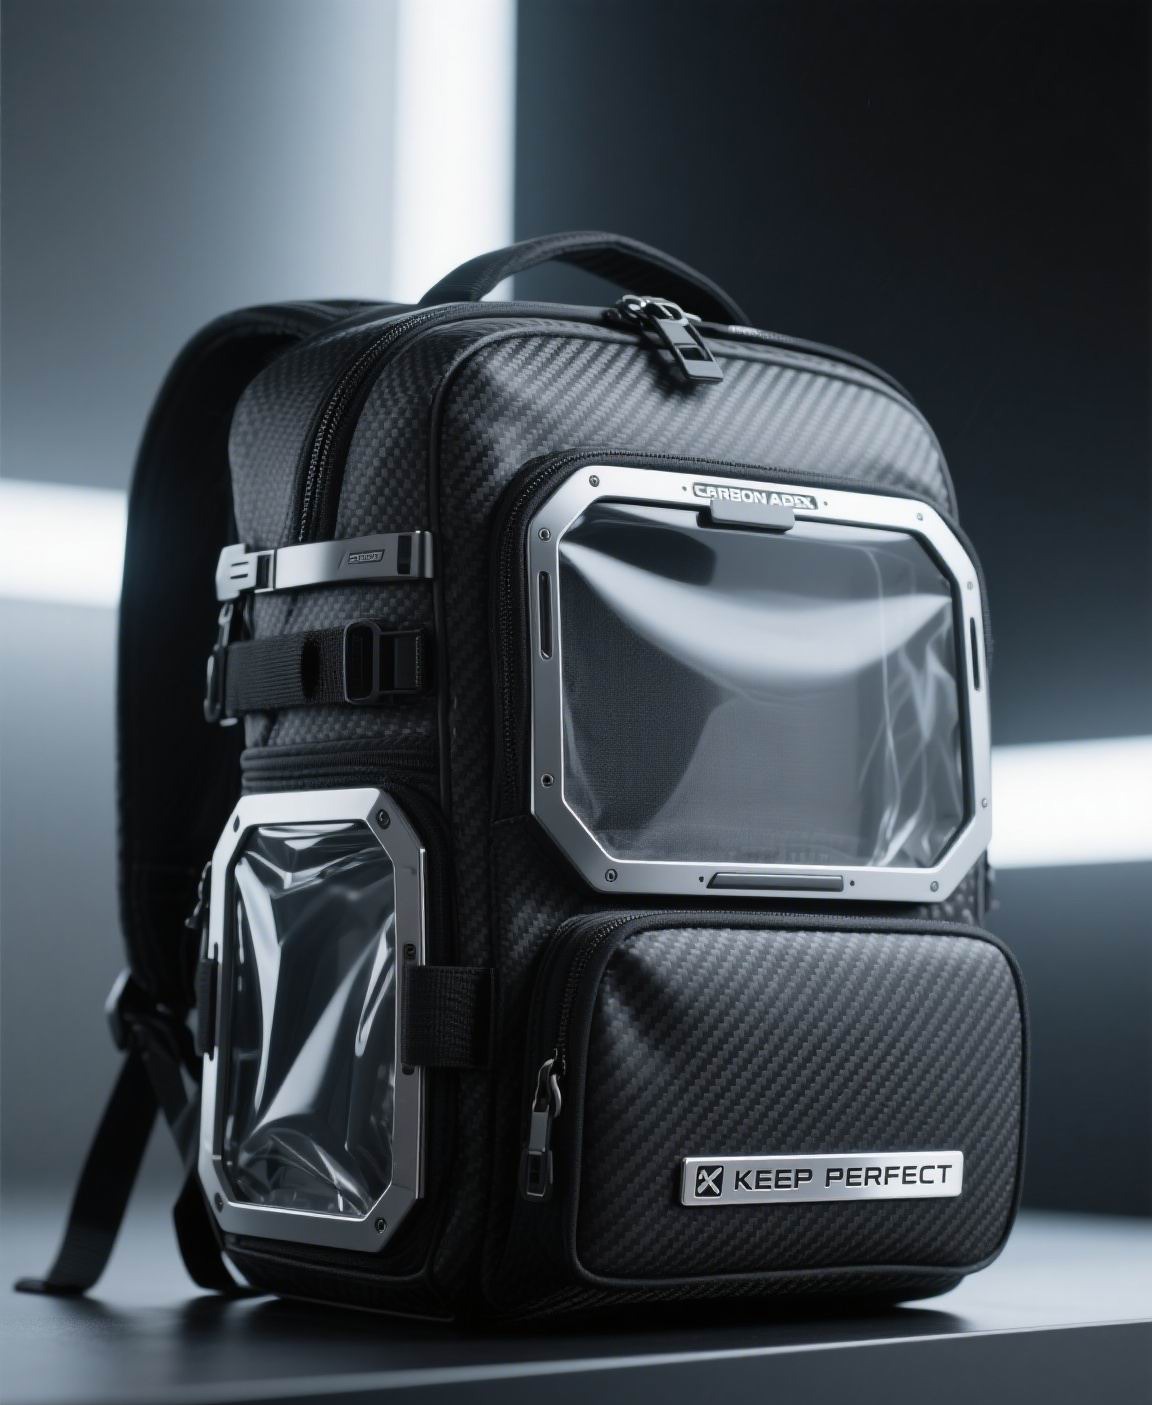
A profitable wholesale order of modular bags is decided by carton geometry, barcode discipline and reorder timing long before it is decided by unit price. A buyer who has 20GP at roughly 28 CBM and 40HQ at roughly 68 CBM available, and who knows the packed carton volume of one modular set, can calculate the freight cost per unit in minutes; a buyer who has not done that arithmetic is negotiating blind. Minimum order quantity sits at 500 units per specification, inspection is run at AQL 2.5, and settlement is T/T 30/70 against FOB Xiamen. The sections below work through carton engineering, labelling obligations, assortment depth, replenishment cadence, inspection at scale, and the freight choices that follow from each.
Carton board grade, stack strength and barcode verification are treated here as specification items rather than as packing-room detail, because each one decides whether a delivery is received or turned away at the dock.
What a wholesale order contains that a project order does not
A project order is bought for one purpose and one delivery date: a conference, a staff rollout, a seasonal campaign. A wholesale order is bought to sit in a distribution centre and be drawn down by stores over months, and that difference changes almost every specification decision. The unit is no longer just a product, it is an inventory item with a barcode, a carton quantity, a shelf presentation, and a reorder trigger.
Start with the master pack. Retail receiving is organised around the case, not the piece. A store back room with limited space wants a carton it can cut open, place on a shelf, and empty without repackaging. That argues for a master-pack quantity tied to the shelf facings a planogram allocates, commonly four, six or twelve units, rather than the largest quantity that fits the carton. Overpacking saves a little in corrugated cost and costs a lot in store labour.
The second difference is assortment. A project order has one specification. A wholesale order usually has several: two or three colourways, perhaps two sizes, and possibly a pouch variant. Each specification variant carries its own minimum, and the arithmetic of how many variants a buyer can afford to open is one of the first decisions in the programme. Minimum order quantity is 500 units per specification, so three colourways at 500 each is a 1,500-unit opening commitment, not a 500-unit one.
The third difference is documentation. Retail receiving desks reject cartons without scannable barcodes, correct origin marking, and a carton label that matches the advance shipping notice. A project buyer shipping to one office can survive a labelling error. A wholesale buyer shipping into a chain's distribution network cannot: the carton is turned away at the dock and the cost of the reverse logistics exceeds the value of the goods.
Finally, the time horizon differs. A project ends. A wholesale programme is expected to repeat for years, which means decisions about fabric continuity, hardware continuity and spare-part availability have to be made up front and written down. A modular platform is well suited to this, because the interface stays constant while modules change, so a reorder two years later still fits the accessories already on the shelf.
Selection rule: Write the assembly reference, pack-out and channel labelling down at the first order and keep the interface constant thereafter, because wholesale only rewards modularity when accessories shipped two years ago still mount on the reorder.
Carton engineering and container arithmetic
Carton dimensions are the cheapest place to lose money in a wholesale programme and the easiest place to save it. Corrugated cost is roughly proportional to board area, freight cost is proportional to volume until the container is full, and both are decided by three numbers: length, width, and height of the master carton. A carton 20 mm too tall, multiplied across a container, is a measurable percentage of the freight bill.
The governing constraint is the packed volume of the product. Modular sets pack worse than flat bags because pouches and straps create void. Compress the shell, nest the pouches inside it where the design allows, and the packed height drops substantially compared with shipping each element separately. Ask the production side for the packed carton dimensions on a real production sample rather than estimating from the flat pattern; estimation is where the error enters.
| Carton option | Units per carton | Packed carton volume | Container fill and consequence |
|---|---|---|---|
| Shell and pouches nested, six per carton | 6 | About 0.072 CBM at 600 × 400 × 300 mm | Roughly 380 cartons in a 40HQ; lowest freight per unit, best store handling |
| Shell and pouches bagged separately, six per carton | 6 | About 0.096 CBM at 600 × 400 × 400 mm | Roughly 290 cartons in a 40HQ; more void, protective for delicate trim |
| Flat packed, twelve per carton | 12 | About 0.060 CBM at 600 × 400 × 250 mm | Highest count per container but requires store assembly and an instruction insert |
| Single unit retail carton, one per carton | 1 | About 0.024 CBM at 400 × 300 × 200 mm | Only viable for courier or air top-up; freight per unit is several times sea |
Container arithmetic follows directly. A 20GP holds about 28 CBM of usable volume, a 40HQ about 68 CBM, and real loading achieves 85 % to 90 % of theoretical because of carton orientation, door clearance and weight distribution. Divide the usable figure by the packed carton volume and then apply that efficiency factor, rather than dividing the nominal container volume and assuming perfection.
Weight matters alongside volume. A container is limited by mass as well as by space, and dense products such as a hardware-heavy modular shell can hit the payload limit before the volume limit. Calculate both and design to whichever binds. Where weight binds, the lever is usually the corrugated grade rather than the product.
Stack strength is the last carton decision. A carton at the bottom of a stack carries the load of everything above it for weeks in a humid container. Specify the board grade and the stacking height the carton must survive, and have it tested, because a collapsed pallet at destination is a total loss rather than a partial one.
Verdict: Specify the board grade and the stacking height the carton must survive and have both tested, since corrugated cost tracks board area and a pallet that collapses after a 25-35 day crossing turns a saving into a write-off.
Barcodes, origin marking and the compliance file
A retail barcode is not a decoration. It is a licence to move through a supply chain, and a carton or a unit without a valid, unique, scannable code will be relabelled at the receiver's expense and charged back to the supplier. The governing system is GS1: a buyer obtains a company prefix, assigns a GTIN to each trade item and each level of packaging, and the codes must be unique across the whole supply chain, not merely within one catalogue.
Three levels usually need codes on a modular programme. The consumer unit carries the retail barcode, typically EAN-13 or UPC-A depending on the market. The master carton carries a different GTIN, usually an ITF-14 printed on the carton label. The pallet carries a serial shipping container code where the retailer requires it. Reusing the unit code on the carton is the most common error and it breaks scanning at the distribution centre.
Print quality is specified, not assumed. A barcode must meet a verified print grade, and it must be tested after the label is applied to the actual curved or textured surface rather than on a flat test sheet. A code printed on a woven label sewn over a seam can fail verification even though the artwork was correct. Ask for a verification report from the production sample, not from the artwork file.
| Document or marking | Issued by | What it must carry | Failure that stalls receiving |
|---|---|---|---|
| GTIN assignment record | The brand owner, from a GS1 prefix | One unique code per trade item and per pack level | Duplicate or reused code; carton scanned as a unit |
| Carton label with ITF-14 | Production side, from buyer data | Carton GTIN, quantity, purchase order, country of origin | Missing purchase order reference; dock cannot match the ASN |
| Country of origin marking | Production side, on the sewn label | Wording required by the destination market | Origin on the carton only, absent from the product |
| CPSIA and California Prop 65 statements | Brand owner, supported by test reports | Applicable declarations for the destination state or country | Declaration absent for a restricted substance in a trim |
| REACH (EC 1907/2006) declaration | Supply chain, consolidated by the production team | Statement on substances of very high concern above 0.1 % | No declaration for a dyed lining or coated shell |
| OEKO-TEX Standard 100 certificate | Textile supplier, referenced to article | Certificate number matching the actual fabric article | Certificate for a different fabric weight than shipped |
| Pre-shipment inspection report | Appointed inspector | ISO 2859-1 sample size with AQL 2.5 result | Report without the sampling standard or the defect counts |
Restricted-substance compliance is a documentation exercise as much as a chemistry one. REACH (EC 1907/2006) governs the European market, California Prop 65 and CPSIA govern parts of the United States market, and OEKO-TEX Standard 100 is frequently requested by retailers as shorthand for textile safety. Each needs a document that references the specific article actually shipped, and a certificate for a different fabric weight is not a certificate.
Nickel release under EN 1811 is worth adding where metal hardware touches skin, because it is a common failure point on buckles and press studs and it is cheap to test relative to the consequence of a recall. Add colour fastness under AATCC 8 for dark colourways, since crocking complaints are a retail return driver that no amount of design quality offsets.
Assortment depth: how many variants a programme can carry
Assortment depth is where wholesale programmes quietly fail. Each additional colourway multiplies inventory risk, because demand across colours is never evenly distributed and the slow colours do not disappear; they sit in a distribution centre consuming working capital and eventually get discounted.
The constraint is the minimum. At 500 units per specification, opening with four colourways means committing to 2,000 units before a single sell-through figure exists. Most first-season wholesale programmes are better served by two colourways plus a strong second drop, because the second drop can be informed by actual data and the first cannot.
The modular structure gives a partial escape from this trap. If the shell is the expensive committed item and the pouches are the cheap variable ones, a buyer can commit to one or two shell colours and offer four or five pouch colours. Customers perceive a wide assortment, the working capital sits mostly in the slow-moving shell, and the pouch reorder is smaller and faster to turn around. This is the single strongest commercial argument for a modular platform in a wholesale context.
Size runs are the second depth decision and behave differently. Unlike apparel, bags have weaker size economics, because most buyers accept one or two capacity options rather than a graded run. Offering 22 litre and 32 litre versions of the same shell is usually enough; a third size rarely earns its inventory. Where a retailer insists on a third, it should be exclusive to that retailer so the slow inventory sits in one place.
Set a kill rule before the first drop ships. Define the sell-through percentage and the time window at which a colourway is discontinued, and write it into the programme plan. Without a rule, the decision gets made emotionally in a range review, which usually means it gets made late.
Bottom line: Set colourway count against how the 500-unit floor divides rather than against enthusiasm, and write the discontinuation rule into the programme plan before the first season ships, because unwritten rules get applied emotionally and late.
Replenishment cadence: turning sell-through into a purchase order
Replenishment timing is arithmetic and it is unforgiving. The pipeline from a purchase order to goods on a shelf is the sum of sampling or approval time, the production window, and the freight transit, and each component has a fixed minimum. Working backwards from the date stock is needed is the only reliable way to place an order.
Standard figures: a sample takes 6–10 working days, or 12–15 where the construction is complex; the production window is 35–50 days from an approved sample; transit is 25–35 days by sea, 5–8 days by air, or 3–5 days by courier. A replenishment order placed on sea freight therefore needs roughly 60 to 85 days of pipeline before the goods can be received, plus the receiving and distribution time inside the buyer's own network.
| Stage | Elapsed time | Days before the shelf date | Decision that must be locked |
|---|---|---|---|
| Sell-through review triggers the reorder | 1–2 days | Day 0 of the cycle | Quantity per colourway, taken from weeks-of-supply arithmetic |
| Order placement and deposit | 1–3 days | About 80 days out | Deposit released under T/T 30/70; fabric reserved |
| Sample or approval reference, if the spec changed | 6–10 working days, complex 12–15 | About 75 days out | Any change in fabric, colour or hardware confirmed |
| Production window | 35–50 days | About 60 days out | Production slot booked, not merely requested |
| Inspection and release | 3–5 days | About 15 days out | AQL 2.5 result and balance payment |
| Sea transit and port handling | 25–35 days plus clearance | About 10 days out | Booked vessel and complete documentation set |
| Distribution centre to store | 5–10 days | Shelf date | Carton quantity matched to store allocation |
Avoid the single most common error: reordering on air freight because the sea window was missed. Air freight runs 5–8 days and courier 3–5 days, which feels like the solution, but air cost per unit on a bulky bag can exceed the unit's gross margin. The correct response to a missed sea window is a smaller air top-up sized to cover only the peak weeks, with the balance following by sea.
Weeks-of-supply is the right trigger metric, not units. Convert current stock to weeks at the recent selling rate, add the pipeline duration, and reorder when the sum approaches the safety stock level. A buyer using this method places orders on a rhythm; a buyer working from a gut feel alternates between stockouts and clearance.
Takeaway: Convert sell-through into orders by comparing weeks of cover against the whole pipeline, counting 6-10 working days of approval time, 35-50 days of production and 25-35 days of sea transit, rather than reordering from instinct and alternating between stockouts and clearance.
Inspection at wholesale scale
Wholesale volumes make inspection both more important and more mechanical. At 2,000 units nobody opens every carton, so the result depends entirely on the sampling plan being correct and the defect classification being agreed in advance. ISO 2859-1 with AQL 2.5 for major defects is the standard commercial arrangement; MIL-STD-105 is the historical predecessor and appears in older specifications, but the current reference is ISO 2859-1.
Classification is where disputes start. Write the defect list before production, with each defect assigned to critical, major or minor, and give the inspector a physical reference sample. A critical defect on a modular product is one that makes the product unsafe or unusable: a fitting that releases below the specified load, a broken needle fragment, a sharp edge on hardware. Major defects are functional or appearance failures a customer would reject. Minor defects are things a customer would tolerate.
Add a functional check that visual inspection misses. On a modular product, the attachment field is the functional surface: a gauge should pass through the webbing rows with a defined force on every sampled unit. A misaligned 25 mm webbing field with 38 mm row spacing will pass a visual check and fail in a customer's hands, which is exactly the outcome inspection exists to prevent.
Decide in advance what happens on a failed lot. The options are a full re-sort at the production site, a rework, or a negotiated concession with a price adjustment. Agreeing this before the failure is worth more than any other clause, because a failed inspection with no pre-agreed remedy turns into a negotiation conducted under time pressure, which is where bad commercial decisions are made.
Inspection also has a cost side worth planning. A standard inspection day covers a defined number of units and a defined scope; adding a functional gauge check or a barcode verification extends the day. Budget for the extended scope rather than discovering at the inspection that the gauge was not included, and insist that the report states the sampling standard, the sample size, and the defect counts by class, because a report without those three items cannot support a commercial decision.
Retained samples close the loop. Ask for three units from the passed lot to be held by the production side against the programme reference. When a customer complaint arrives eight months later, the question is almost always whether the shipment differed from the approval, and a retained sample answers it in an afternoon rather than over several weeks of correspondence.
Judgement: Fix the sampling plan and the defect classification before production and hold a retained sample per lot, because months later the argument is whether the shipment differed from the approval and one reference answers that in an afternoon.
Freight, settlement and the documents that move with the goods
Standard settlement on this programme is T/T 30/70, with 30 % released to start the production slot and 70 % against a passed inspection and release of the shipping documents, quoted FOB Xiamen. Buyers new to the arrangement should note what FOB means in practice: the seller's responsibility ends when the goods pass the ship's rail at the named port, and everything after that, including the ocean freight, insurance and destination handling, is the buyer's account.
Freight mode is chosen from the calendar and the margin. Sea freight at 25–35 days is the default for planned replenishment. Air at 5–8 days is for a genuine stockout or a launch date that moved. Courier at 3–5 days is for samples and for small top-ups measured in tens rather than hundreds of units. Where IATA dangerous-goods rules could apply to any component, check before booking; most bag programmes are unrestricted, but magnetic closures and lithium accessories occasionally trigger questions.
Consolidation is worth considering for smaller replenishments. A buyer whose reorder does not fill a container pays less-than-container-load rates, which are higher per cubic metre and involve more handling, and therefore more damage risk. Consolidating two reorders into one shipment every other cycle often saves more than the extra inventory carrying cost.
Documentation must travel with the right timing. The commercial invoice, packing list, bill of lading and any certificates of origin have to reach the buyer's broker before the vessel arrives, not after. A container sitting at a port accruing demurrage because a certificate was late is a pure loss, and it is the most avoidable cost in the whole programme.
Capacity planning belongs in the same conversation. A programme that settles into a quarterly rhythm should be telling the production side its annual volume, because fabric and hardware lead times are long and a reserved slot behaves differently from a negotiated one. Our 4,950 m² SGS-verified production floor runs 7 production lines with 137 people and 149 machines at 200,000 units per month, and a wholesale buyer sharing a rolling twelve-month forecast gets fabric reserved against it rather than competing for it each cycle.
Finally, treat the first drop as a controlled experiment. Ship it, measure sell-through by colourway, record the damage rate on arrival, and note every customer comment that mentions fit, mounting force or pouch position. Those three data sets are what turn the second drop from a repeat order into an improvement, and a modular platform is unusually forgiving here because the interface can stay fixed while the module mix is corrected.
Spec rule: Settle FOB Xiamen under T/T 30/70 with the 70% leg tied to a passed inspection and released shipping documents, since every recurring complaint becomes a line item that the next drop can correct only if something is held back until it passes.
Frequently asked questions
What is the minimum order quantity for a wholesale modular programme?
Minimum order quantity is 500 units per specification. That means each colourway and each size variant counts separately, so opening with three colourways commits the buyer to 1,500 units rather than 500. Plan the first drop around two colourways and use actual sell-through to shape the second.
How many units fit in a 40HQ container?
Divide usable volume by packed carton volume and apply a loading efficiency of 85 % to 90 %. A 40HQ offers about 68 CBM and a 20GP about 28 CBM. At 0.072 CBM per six-unit carton that is roughly 380 cartons, or about 2,280 units, before the payload limit is checked.
Should I ship the pouches inside the shell or separately?
Nesting pouches inside the shell reduces packed volume by roughly a quarter compared with bagging them separately, which lowers freight per unit directly. Bag them separately only where trim is delicate enough that contact damage outweighs the freight saving.
Do I need a separate barcode for the carton?
Yes. The consumer unit carries an EAN-13 or UPC-A, and the master carton carries a different GTIN, normally an ITF-14 on the carton label. Reusing the unit code on the carton breaks scanning at the distribution centre and will be charged back.
Who owns the GS1 prefix and the code assignment?
The brand owner obtains the company prefix and assigns the GTINs, then supplies them to the production side for printing. Codes must be unique across the entire supply chain, not just unique within one catalogue, and the assignment record should be kept as part of the programme file.
What compliance documents does a retail chain ask for?
Expect a REACH (EC 1907/2006) declaration, California Prop 65 and CPSIA statements for the United States, an OEKO-TEX Standard 100 certificate referenced to the actual fabric article, and a pre-shipment inspection report citing ISO 2859-1 at AQL 2.5. Add EN 1811 nickel release where metal hardware touches skin.
How far ahead should a sea replenishment order be placed?
Work backwards from the shelf date. Allow 6–10 working days for a sample if the specification changed, 12–15 where complex, then a 35–50 day production window, then 25–35 days of sea transit, then clearance and internal distribution. In practice that is roughly 80 days from order placement to shelf.
When is air freight justified on a restock?
Almost never for the full quantity. Air runs 5–8 days and courier 3–5 days, but air cost per unit on a bulky bag can exceed the gross margin. Use air for a top-up sized to cover only the peak weeks and let the balance follow by sea.
What carton quantity should I specify?
Match it to the planogram. Four, six or twelve units per master carton lets a store cut open and shelf the contents without repackaging. Maximising units per carton saves a little corrugated and costs substantially more in store labour.
How is a failed inspection lot handled?
Agree the remedy before production: full re-sort at the production site, rework, or a documented concession with a price adjustment. A pre-agreed clause is worth more than any other part of the inspection plan, because a failure without one becomes a negotiation under time pressure.
What settlement terms apply on a bulk order?
Standard terms are T/T 30/70 quoted FOB Xiamen: 30 % released to open the production slot and 70 % against a passed inspection and release of shipping documents. Under FOB the buyer carries ocean freight, insurance and all destination handling from the named port.
How do I avoid being caught by stack strength failures?
Specify the board grade and the stacking height the carton must survive, then have it tested. Cartons at the bottom of a stack carry everything above them for weeks inside a humid container, and a collapsed pallet is a total loss rather than a partial one.
Is it better to consolidate two small reorders?
Usually yes. Less-than-container-load rates are higher per cubic metre and involve more handling, which raises damage risk. Combining two cycles into one full container typically saves more than the additional inventory carrying cost.
Why keep shell colourways narrow and pouch colourways wide?
Working capital sits in the shell. Committing to one or two shell colours at 500 units each while offering four or five pouch colours gives customers a wide perceived assortment while keeping most of the inventory risk in cheap, fast-turning items.
What should a kill rule for a colourway contain?
A sell-through percentage, a time window, and the action that follows. Define them before the first drop ships so the decision is made against data rather than in a late range review where it is usually made emotionally and too late.
Do magnetic closures affect freight booking?
Occasionally. Most bag shipments are unrestricted, but magnetic fittings and any lithium accessory can prompt questions at booking under IATA rules. Declare them when booking air freight rather than having a shipment held at the airport.