Home › Field notes › Own-Brand Modular Programme: Identity, Tooling and Launch Gates
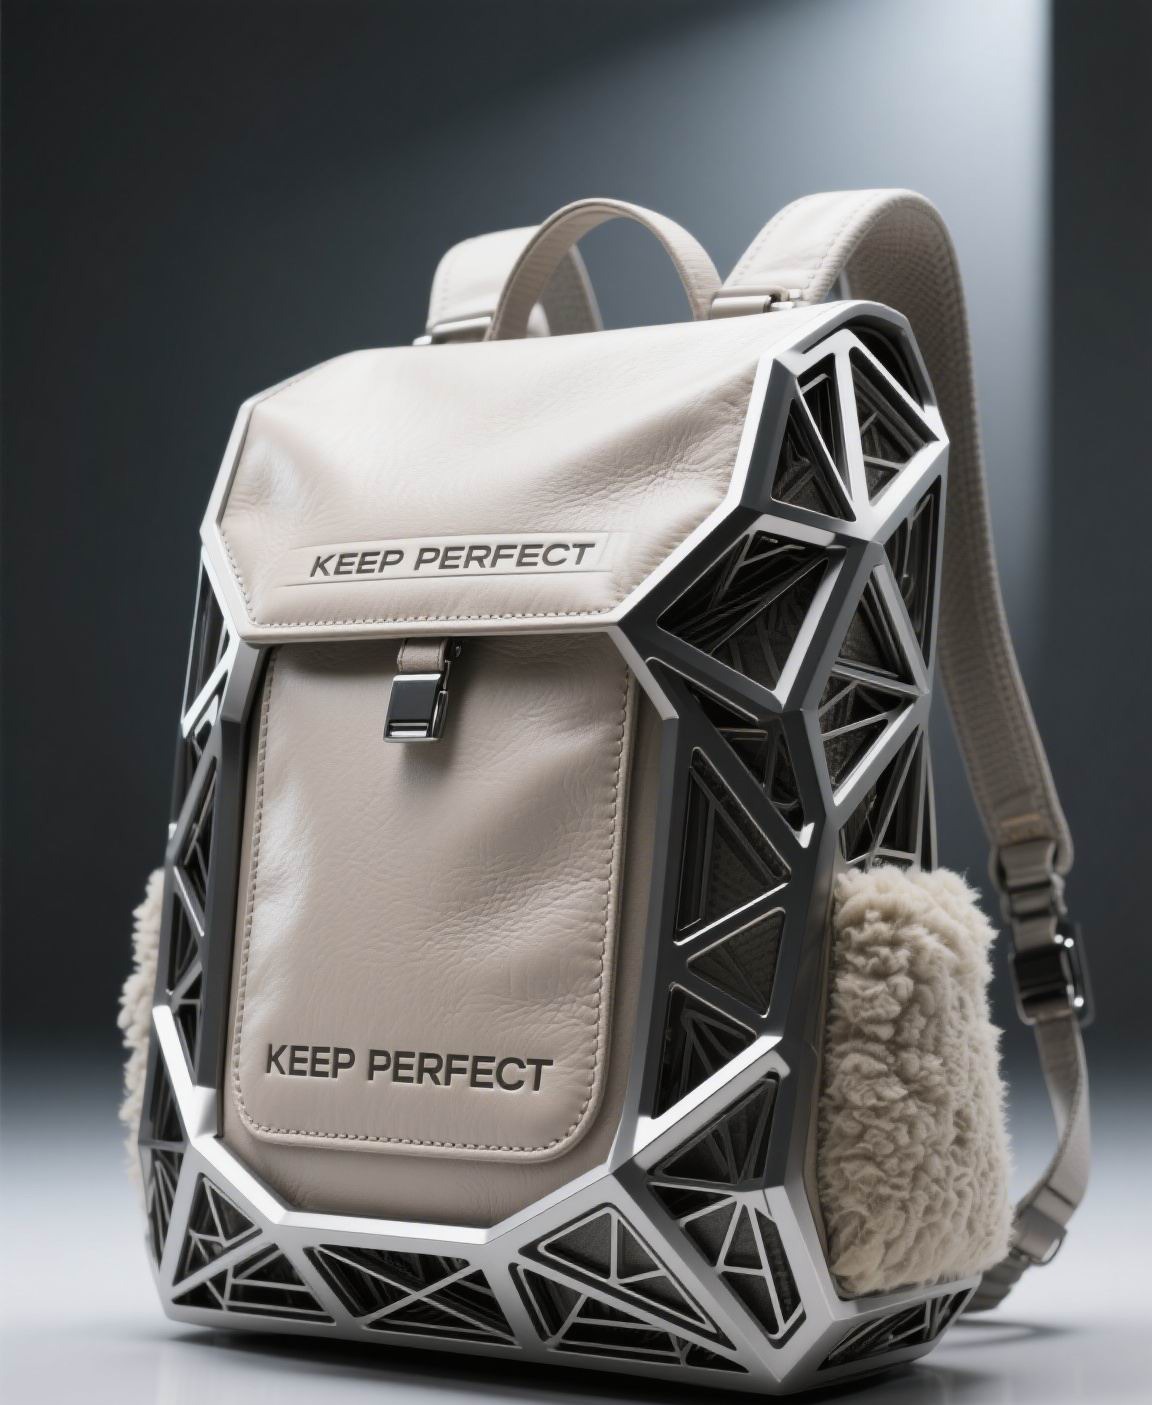
An own-brand modular programme buys three things a bought-in range cannot: control of the attachment interface, control of the identity surfaces, and control of the replenishment cadence. Everything else follows from those three. Interface control starts with one geometric rule, 25 mm webbing at 38 mm of row spacing and a 50 mm sideways repeat, and it is what keeps a module released in year three fitting a chassis sold in year one. Identity control is a wear problem before it is a design problem, because a mark placed on a strap fold abrades away in a season. The commercial frame is fixed: MOQ 500 per reference, sampling at 6-10 working days, tooling and screens at USD 300-2,500, and release held at AQL 2.5. The sections follow the order a brand meets them: what the interface commits, where a mark can survive, what setup costs, then how the first pallet is scheduled. Brand identity on a modular product is therefore a specification problem long before it is a design one.
What an own-brand modular programme actually buys
Two routes sit in front of a brand entering this category. The first is to buy an existing range, apply a mark to it and sell it. The second is to define the product: the chassis geometry, the attachment rule, the module set and the identity surfaces. The first route is faster and cheaper to start, and it leaves the brand with nothing it owns. The second takes longer and produces an asset that appreciates, because every module released later strengthens the platform.
The commercial difference shows up in margin structure rather than in gross margin. A resold chassis earns one margin event. A defined chassis earns a margin event at the base sale and then again at each accessory purchase, and accessory attach rates on well-executed modular ranges routinely exceed thirty per cent within a year of launch. That compounding is unavailable on the resale route, because the brand does not control the interface that makes the second sale possible.
Cost is the honest counterweight. Defining a product means paying for pattern work, screens, artwork setup and, where the design requires it, mould tooling. It means writing a specification detailed enough to be inspected, and holding a sample review gate before money moves. It means a longer route to first revenue. Brands that skip this work usually discover the cost later, in the form of a module that does not fit, a mark that peels, or a replenishment that cannot be placed because nobody documented what was actually made.
In industry vocabulary this arrangement is often called a private label programme. The phrase describes the commercial relationship, who owns the mark and who sells the unit, and it says nothing about the engineering. A brand can hold a private label arrangement over a completely generic product or over a fully defined one, and the difference in outcome is entirely in the specification work that sits behind the label.
Selection rule: Selection rule: Decide what the brand mark must survive before choosing where to place the mark, because placement on a high-abrasion panel costs more in returns than placement on a protected one ever costs in visibility, and the decision has to hold for a run of 500 units.
Identity surfaces: where a brand mark survives and where it fails
A brand mark on a bag is a wear component. It sits somewhere, that somewhere has a duty cycle, and the process used to apply it either survives that duty cycle or does not. Treating the mark as artwork rather than as a component is the most common reason a launch range looks tired after one season, and the fix is inexpensive if it happens at the brief stage and expensive if it happens after the first return.
Six zones carry a mark on a modular chassis, and they behave very differently. A flat front panel sees abrasion from surfaces and from conveyor belts, and it tolerates almost any process. A shoulder strap sees flexing and continuous rubbing against clothing, which kills stiff transfers. A zipper pull sees constant handling and chemical contact from hands, which attacks painted finishes. A lining sees whatever the customer carries, plus sanitiser residue. Hardware sees impact and corrosion. Packaging sees warehouse handling and is the cheapest place to carry detail that would not survive on the product itself.
Process selection follows from that. Woven labels survive flexing but add a seam and a potential leak path. Silicone patches survive abrasion and wipe-down but need a flat, stable substrate and a clean edge radius. Heat transfers give fine detail and fail at the edge once the substrate flexes. Embroidery reads as premium and snags on webbing edges. Metal badges look expensive and concentrate corrosion risk at the plating edge. Each of those is a defensible choice in the right zone and a predictable failure in the wrong one.
| Placement zone | Decoration route that suits it | Load it must survive | Setup line opened |
|---|---|---|---|
| Flat front panel | Woven label or silicone patch | Surface abrasion and conveyor contact | Digitising or mould, one per artwork |
| Shoulder strap | Woven label, sewn not transferred | Continuous flex and clothing rub | Second marker position in the pattern |
| Zipper pull | Laser mark or moulded pull | Handling plus residue from hands | Pull tooling, shared across colourways |
| Lining face | Woven label at a seam | Contents abrasion and wipe-down | Lining marker revision |
| Hardware plate | Etched or domed metal | Impact and salt exposure | Badge tooling plus corrosion check |
| Retail packaging | Printed carton and insert | Warehouse handling and stacking | Print plates, lowest setup of the six |
Verification closes the loop. Require an abrasion check to ISO 12947 on the marked panel, a crock check to AATCC 8 on any printed surface, and a corrosion check to ASTM B117 on any metal component. Those three tests cost a fraction of a rework and remove the argument entirely, because the evidence either exists or it does not.
Setup cost lines and what each one actually buys
Setup cost is the line that most first-time budgets understate, and it is also the line most easily misunderstood as a fee rather than as a purchase. Screens, dies, embroidery digitising and mould tooling are durable assets. They exist after the first order, they are reused on the second, and they are the reason a follow-on run quotes lower than an opening run.
The band is wide because the content varies. Reusing an existing pattern with a new artwork sits at the bottom of the range and mostly buys screen setup and digitising. Introducing a moulded panel, a custom pull or a welded module sits at the top and buys steel that will be amortised over several years. What matters for planning is to separate the one-time lines from the per-colourway lines, because only the second group scales with the number of variants in the range.
| Expenditure line | Trigger that opens it | Typical band | Lever that moves it |
|---|---|---|---|
| Pattern and marker work | New chassis geometry | Within the USD 300-2,500 setup band | Sharing one chassis across several references |
| Screen and plate setup | New artwork or new print position | Low end, scales per colourway | Limiting artwork positions on the tech pack |
| Embroidery digitising | Stitched mark rather than woven | Low end, one per artwork | Standardising one mark across the range |
| Hardware tooling | Custom pull, badge or buckle | High end of the same band | Using a stock component in a brand finish |
| Sampling fee | First reference sample | USD 50-150, refunded on order | Closing the brief before requesting a sample |
| Compliance testing | Destination market requirement | Varies by market and material set | Reusing a qualified material across colourways |
Amortisation is the arithmetic that decides whether the spend is sensible. Across 500 units a setup band of USD 300-2,500 adds somewhere between sixty cents and five dollars a unit. Spread over 2,000 units the identical spend adds between fifteen cents and a dollar twenty-five. That difference is the entire argument for planning a second run before the first one ships, and it is why the opening buy should be sized to reach the follow-on rather than optimised for its own unit price.
Bottom line: Bottom line: Separate one-off setup charges from unit price on every quotation, and compare two quotations only after both have listed tooling and screens in the USD 300-2,500 band and the sampling fee at USD 50-150 as separate lines.
Interface ownership as the durable brand asset
Of the three things an own-brand programme buys, interface ownership is the one competitors cannot copy cheaply. A colourway is copied in a season. A silhouette is copied in two. An interface, once a brand's module catalogue depends on it and customers own three or four pouches built to it, creates a switching cost that lasts years.
The grid published on this site is 25 mm webbing, 38 mm of row spacing and a 50 mm sideways repeat. Adopting that as the brand's declared rule delivers immediate compatibility with a large installed base of pouches, which solves the cold-start problem: a launch chassis is useful on day one because customers may already own accessories that mount to it. Layering a brand-owned fitting on top delivers differentiation where it is actually experienced, at the module the brand sells and at the release action the customer performs.
Two rules keep that asset intact. First, version the interface: every module declares the version it targets, every chassis declares the versions it accepts. Second, tolerance the spacing rather than stating a nominal figure, because a repeat that drifts two millimetres across a panel will takes a pouch on a table and binds in service once the panel is loaded and slightly stretched. Both rules cost nothing to write and prevent the most expensive modular failure there is, a silent geometry change that strands an accessory catalogue.
Our production team treats the interface drawing as a controlled document rather than as a reference image, which is what allows a reorder two years later to match the original mounting behaviour. That discipline belongs to the brand as much as to the line: the drawing should live in the brand's specification set, not only in the supplier's folder, because the brand is the party with the commercial interest in continuity.
Verdict: Verdict: Treat the published interface as the durable asset and the chassis as the depreciating one, and keep the grid at 25 mm webbing and 38 mm row pitch across every revision so earlier pouches keep fitting later shells.
Colourway architecture and the SKU discipline behind it
Colourway count is the fastest way to destroy the economics of a launch range. Each additional colourway adds a marker, a thread and trim set, a shade-matching check and an inspection line, and it fragments a 500-unit buy into runs too small to reveal anything. Two colourways is usually the right answer for a first buy; three is defensible when the channel is broad; five is a decision to buy information at a price that rarely pays back.
SKU discipline matters as much as colourway count, because modular ranges generate codes faster than conventional ones. A chassis, three modules and two colourways is already six sellable units before packaging variants. Without a coding scheme, the second order becomes an exercise in archaeology, and the reorder goes to the wrong component.
| SKU field | What it encodes | Error it prevents | Owner of the field |
|---|---|---|---|
| Platform prefix | Chassis family and interface version | Ordering a module against the wrong grid | Brand, fixed at brief close |
| Capacity band | Nominal volume in litres | Shipping a size the channel did not list | Brand, from the range plan |
| Colourway code | Shell colour and trim colour | Mixed trim on a single retail order | Brand, locked at sample approval |
| Module suffix | Module type and mounting tier | Reordering a pouch that will not mount | Brand, from the interface register |
| Revision digit | Pattern revision currently in build | Building an obsolete revision by default | Production team, updated per change |
| Market suffix | Destination and labelling variant | Shipping the wrong compliance labelling | Brand, from the market plan |
The revision digit is the one field most schemes omit and the one that causes the most damage. Without it, a change made in month eight silently becomes the default build, and a year later nobody can say whether the units in the warehouse accept the modules on the shelf. Adding one character to the code removes that ambiguity permanently.
Packaging, labelling and the compliance file
Packaging fails programmes late and expensively, because it is specified last and discovered at the dock. A retail receiver will reject a shipment for a barcode that does not scan, a carton marking that disagrees with the paperwork, or a missing fibre-content statement, and none of those defects has anything to do with the quality of the bag. Specifying packaging alongside the product rather than after it removes an entire class of delay.
Labelling content is market-specific and should be settled before the artwork is finalised. A United States destination brings CPSIA considerations for any product positioned for children and California Prop 65 warnings where a listed substance is present above a threshold. A European destination brings REACH (EC 1907/2006) substance restrictions and, where a claim is made, documentation to support it. Fibre content, country of origin and care symbols are routine but must be correct, because these are the fields a customs officer and a retail compliance reviewer both check first.
Where a brand wants a textile-safety claim, OEKO-TEX Standard 100 certification on the material set is the usual evidence, and it should be requested against the actual fabric and trim combination rather than against a generic fabric reference. Chemical testing is specific to what was tested. A certificate that names a different construction supports nothing, and a reviewer who notices will treat it as evidence of carelessness rather than as evidence of safety.
Two practical gates close this section. First, require a packaging sample alongside the product sample, so that carton strength, print quality and barcode scannability are approved in the same meeting. Second, require a transit check to ISTA 3A on the packed carton, because a bag that survives the drop test and arrives with a crushed carton still generates a return.
Takeaway: Takeaway: Treat packaging and labelling as part of the compliance deliverable rather than as artwork, and confirm carton markings, fibre content and country-of-origin statements before the print run is released and the pack-out is set to roughly 28 CBM per 20GP.
Commercial terms and where the risk actually sits
Terms are a risk-allocation instrument, not a formality. The standard arrangement for this category is T/T 30/70 on FOB Xiamen terms: thirty per cent on order to release materials and book capacity, seventy per cent against release of the finished goods after final inspection. The first payment buys commitment and materials. The second is contingent on inspection passing, which is what keeps quality leverage in the buyer's hands until the goods are actually finished.
Incoterm choice matters more than most buyers expect. Under FOB Xiamen the seller's obligation ends when goods pass the ship's rail at the named port, and freight, insurance, import duty and onward carriage sit with the buyer. That is a good arrangement for a buyer with a freight forwarder and a predictable lane, and a poor one for a buyer without either. Quoting the arrangement explicitly alongside any indicative price is what prevents the landed-cost surprise that follows a bare unit figure.
Capacity planning is the other side of the same conversation. The 4,950 m² SGS-verified production base we work with runs 7 production lines with 149 machines and a workforce of 137 people, which supports output around 200,000 units per month across the programme. For a brand planning 500 units, that headroom means the constraint is never capacity; it is always the brief, the sample approval, and the material lead time. Knowing which constraint is binding is what makes a schedule credible.
Quality leverage is held at inspection. Release against AQL 2.5 by ISO 2859-1 sampling, with the defect classes defined in the brief, gives both parties a shared decision rule rather than a negotiation at the dock. A modular reference should list mounting fit and spacing as their own defect class, because those fail functionally and a purely visual inspection will pass a panel whose pouches jam.
A hundred-and-twenty-day route from brief to first pallet
The route from a closed brief to goods on a pallet is longer than most first-time planners expect, and almost all of the length is in the parts they control rather than in the build. Working backwards from an arrival date remains the only dependable way to plan it, and doing so early is what turns a launch date into a commitment rather than a hope.
Days one to fifteen belong to the brief and the material decision. Fabric, webbing, hardware and trim selections all have lead times, and a speciality fabric ordered late can add three weeks that no amount of schedule pressure recovers. Closing the brief with the interface drawing, the dimension callouts and the identity placement all fixed is the deliverable that makes everything downstream predictable.
Days fifteen to thirty-five cover sampling, which runs 6-10 working days on a conventional build, widening to 12-15 working days where a moulded part or a welded pouch enters the specification. Sample review, correction and approval realistically consume the remainder of that window, since an initial sample seldom satisfies every requirement. Days thirty-five to ninety hold mass production at 35-50 days from deposit, and days ninety to one hundred and twenty cover inspection, release and freight, which is 25-35 days on the water, 5-8 by air, or 3-5 by express courier.
The discipline that makes this route work is a gate at each boundary: brief closed before sampling starts, sample approved before the deposit moves, inspection passed before the balance is paid, and packaging approved before the cartons are printed. Each gate is cheap to hold and expensive to skip, and each one is a decision the brand owns rather than one it can delegate.
Two references help while the brief is being written: the attachment grid geometry that fixes module compatibility, and the chassis platform the range will sit on.
Spec rule: Spec rule: Allow 6-10 working days for sampling, 35-50 days for production and 25-35 days for sea freight, and sequence artwork approval before the tooling is cut rather than during the production window.
Frequently asked questions
What does an own-brand modular programme actually mean?
It means the brand defines the chassis geometry, the attachment rule, the module set and the identity surfaces rather than buying an existing range. In industry vocabulary this is often described as a brand-owned arrangement, though that phrase covers the commercial relationship only and says nothing about the engineering behind it.
Why is interface ownership the most valuable part?
Because it creates a switching cost. Once customers own three or four pouches built to a brand's declared grid, changing chassis supplier means abandoning that accessory investment. A colourway is copied in a season; a versioned interface is not.
What interface geometry should a brand declare?
Declare 25 mm webbing at 38 mm vertical spacing with a 50 mm horizontal repeat, stated as a tolerance band rather than a nominal figure. That geometry gives immediate compatibility with a large installed base of pouches and solves the cold-start problem at launch.
Where should the brand mark go on a modular chassis?
Flat panels take almost any process. Straps need sewn woven labels because transfers crack under flex. Pulls need laser or moulded marking because painted finishes fail under handling and residue. Packaging is the cheapest place for detail that would not survive on the product.
How much does setup cost on a first modular order?
Budget USD 300-2,500 covering tooling, screens, digitising and pattern work, depending on how much is new. Across 500 units that adds roughly USD 0.60-5.00 per unit; across 2,000 units it drops to roughly USD 0.15-1.25.
Is the sampling fee refunded against the production order?
Yes. The sampling fee is USD 50-150 per reference and is credited back against the order, so a brand that proceeds pays that cost once. It pays for marker work, the cloth drawn for one sample and the labour to assemble it.
How long does sampling take?
Sampling runs 6-10 working days on a conventional build, widening to 12-15 working days where a moulded panel, a custom pull or a welded pouch enters the specification. Sample review and correction typically add a further ten to fifteen days.
How many colourways should a launch range carry?
Two. Each extra colourway adds a marker, a trim set, a shade check and an inspection line, and it fragments a 500-unit buy into runs too small to reveal preference. Three is defensible in a broad channel; five rarely pays back.
What payment terms are standard?
T/T 30/70 on FOB Xiamen terms. Thirty per cent on order releases materials and books capacity; seventy per cent is paid against release after final inspection, which keeps quality leverage with the buyer until the goods are finished.
What does FOB Xiamen place on the buyer?
Under FOB the seller's obligation ends when goods pass the ship's rail at the named port. Freight, insurance, import duty and onward carriage sit with the buyer, so any indicative unit price must always be interpreted as FOB Xiamen at 500 units rather than as a delivered figure.
What inspection standard applies at release?
Release stands at AQL 2.5 using ISO 2859-1 sampling tables, with defect classes written into the brief. Modular references should list interface fit and spacing as a separate defect class, since those fail functionally and pass a purely visual check.
Which compliance documents does a European destination need?
REACH (EC 1907/2006) substance restrictions apply, with fibre content, country of origin and care symbols on the label. Where a textile-safety claim is made, OEKO-TEX Standard 100 evidence must name the actual fabric and trim combination rather than a generic fabric reference.
What should a packaging sample include?
The carton, the print, the barcode and any insert, approved in the same meeting as the product sample. Add an ISTA 3A transit check on the packed carton, because a unit that survives the drop test and arrives in a crushed box still generates a return.
How much capacity is available for a growing programme?
The 4,950 m² SGS-verified production base we work with runs 7 production lines with 149 machines and 137 people, supporting roughly 200,000 units per month. For a 500-unit opening buy, capacity is never the binding constraint; the brief and material lead times are.