Home › Field notes › What Modular Means in Bag Design: Interfaces, Decoupling, Lifecycle
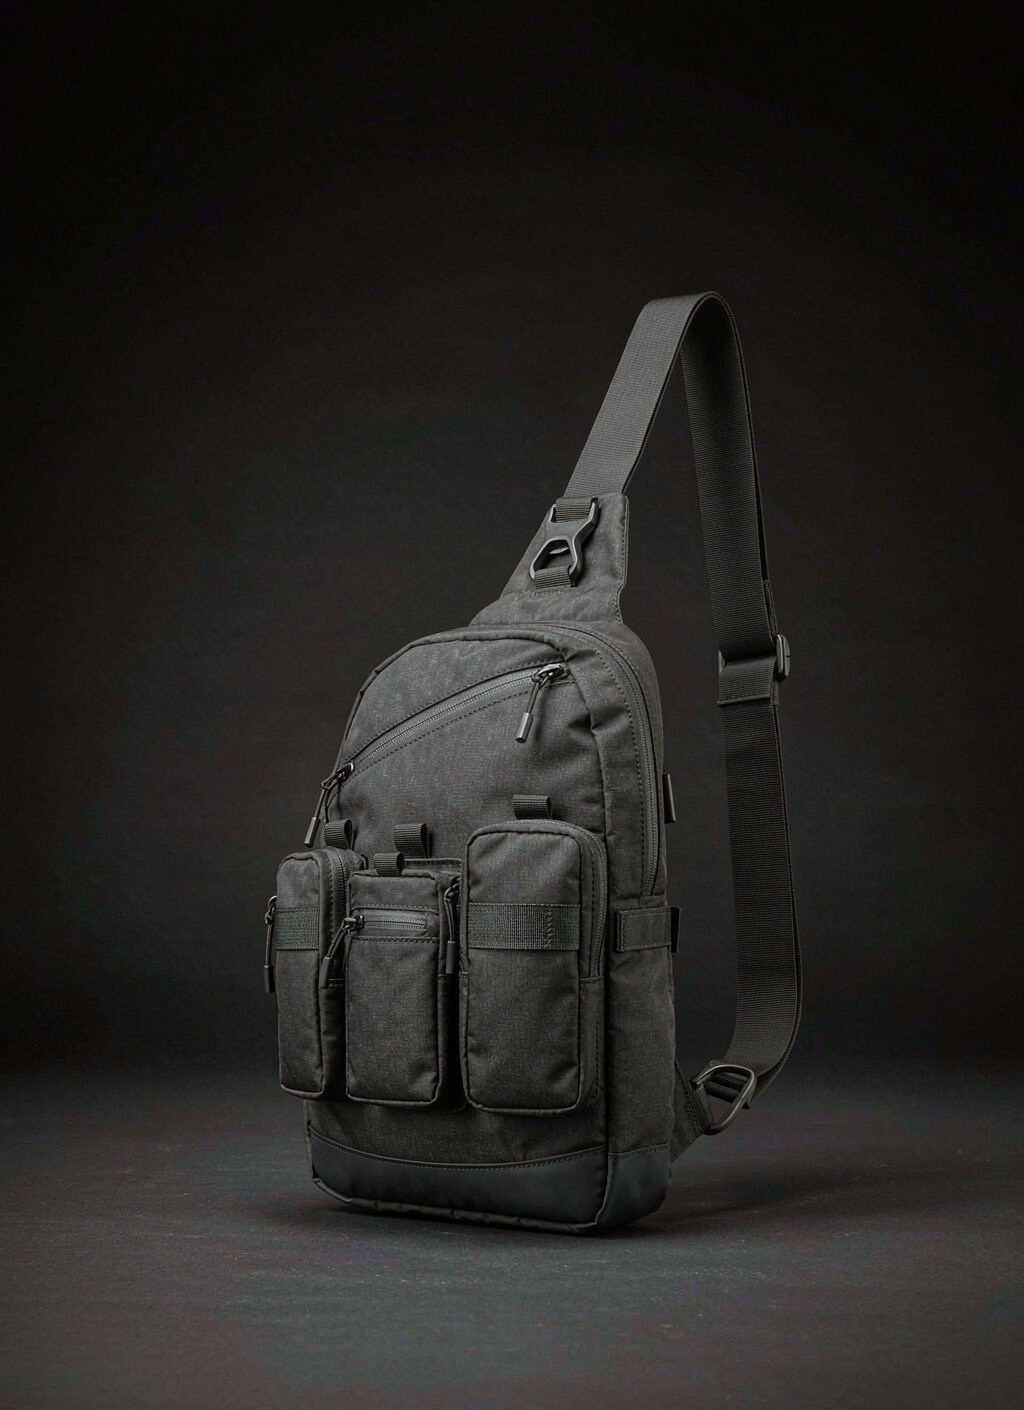
Modular in bag design means that a bag's function is split across parts joined by a declared, standardised interface, so one part can change without forcing the others to change with it. Three properties make that real: an interface written as geometry rather than as a picture, functional decoupling that puts slow-changing properties in the chassis and fast-changing ones in the module, and lifecycle compatibility that keeps a replacement module fitting a carrier bought years earlier. A modular programme runs at MOQ 500 per reference, samples in 6-10 working days and produces across 35-50 days. Civilian scope only: commuting, travel, work tools, trail kits, camera and first-aid modules.
Three meanings of modular, and which one is being sold
The word is used for three different things, and the differences are not academic. Interface-defined modularity means a written geometry binds the parts and a module made next year will fit. Accessory-compatible modularity means the product accepts its own accessories, but the geometry is unpublished and may change without notice. Decorative modularity means the exterior suggests modularity - printed grids, unused loops, panels nothing can mount to - while nothing is actually exchangeable.
Only the first survives a reorder, and that is the practical test. Ask what happens if a module is reordered two years from now against a carrier bought today. If the answer depends on a drawing, modularity is real. If it depends on hope, it is one of the other two.
The second meaning is not worthless. Accessory-compatible products deliver most of the user benefit in the first two seasons and cost less to develop, because nobody has to maintain a contract. The problem is that the benefit quietly stops at the point where the geometry changes, usually without anyone noticing until a customer complains.
The third meaning should be named and avoided in technical copy. A decorative panel is a styling decision and there is nothing dishonest about styling, but describing it as modular in a specification invites a buyer to plan a range around a capability that does not exist. That is where the word causes real financial damage.
Selection rule: Test any modular claim with one question - will a module reordered in two years fit a carrier bought today - and treat a yes that depends on a drawing as real modularity and a yes that depends on hope as styling.
Interface standardisation: the only definition that survives reorder
An interface is standardised when it is written as dimensions with a tolerance and a measurement datum, held under revision control, and referenced by every part that uses it. Those four conditions are individually obvious and collectively rare. Most ranges satisfy two or three of them, which is why most ranges drift.
Geometry comes first. Webbing width, vertical spacing between rows and the repeat of the anchoring pattern are the three numbers that decide whether a strap will fit and how many rows it will engage. Written as 25 mm, 38 mm and 50 mm with a stated tolerance, they are testable; described as a webbing panel in a catalogue, they are not.
Tolerance and datum come next, and they are where arguments start. Two parties can each measure correctly and still disagree, purely because one worked from a row centre and the other from a row edge. Stating the datum on the drawing takes one short sentence, and it ends that disagreement for good.
Revision control is the condition most often skipped. A drawing without a revision number cannot be referenced, so nobody can prove which version a given shipment was built to, and a substitution becomes invisible. Where a programme spans more than one season on a shared modular chassis, revision control is the single cheapest insurance available.
Verdict: Standardise an interface by writing geometry, tolerance and datum under revision control and referencing it from every part drawing, because a drawing without a revision number cannot prove what any given shipment was built to.
Functional decoupling: what belongs in the chassis and what belongs in a module
Decoupling is an allocation decision, and the allocation rule is change frequency. Properties that change slowly - harness fit, shell material, panel stiffness, volume - belong in the chassis, where change is expensive but rare. Properties that change quickly - capacity, organisation, colour coding, accessory function - belong in the module, where change is cheap and frequent. Sorting every element by how often it will change produces the correct split almost automatically.
| Element | Change frequency | Recommended home | Reason for the placement |
|---|---|---|---|
| Harness and back panel | Very low | Chassis | Fit is expensive to redevelop |
| Shell fabric and colourway | Low to medium | Chassis | Drives the visual identity |
| Attachment face geometry | Never within a generation | Chassis | Every module depends on it |
| Capacity and volume | High | Module | The reason modularity exists |
| Internal organisation | High | Module | Changes with the task |
| Colour coding and labelling | High | Module | Used for identification |
| Protective padding | Medium | Module | Tied to the contents |
| Branding execution | Medium | Either | Costume change, no fit effect |
Two allocation mistakes recur. The first is putting volume in the chassis, which means every capacity change becomes a new bag rather than a new pouch. The second is putting protective padding in the chassis, which forces a heavy shell on users who carry nothing fragile. Both mistakes are easy to make because both elements feel structural, and both are expensive to reverse once tooling exists.
Decoupling also has a user-experience dimension. A well-decoupled system lets a user change one thing without re-learning the whole bag: same harness, same placement logic, different module. A poorly decoupled one changes the interface every season and makes every module an unfamiliar object, which is the fastest way to lose the benefit of the whole approach.
Bottom line: Allocate by change frequency - harness, shell and interface geometry to the chassis, capacity, organisation and padding to the module - and never place volume in the chassis, because that turns every capacity change into a new bag.
Lifecycle compatibility: designing for the third season
Lifecycle compatibility asks a simple question with an unglamorous answer: when this range is in its third season, will parts still interchange? Answering yes requires three decisions made early - how generations are numbered, how retired modules are supported, and how spare parts are held.
Generation numbering should be derived from the interface itself. Alter the geometry and the generation number moves; keep the geometry and the number holds, whatever else is revised. That rule converts an invisible drift into a visible event and gives customers a way to know what they hold and what it works with. It also settles the internal argument about whether a harness change counts as a new generation, which it does not, because harness changes do not affect fit.
Retirement needs a published window. When a module leaves the range, stating that spares remain available for a stated number of seasons costs almost nothing and removes the worst kind of support complaint. Silence, by contrast, is read as abandonment by customers who have built a kit around that module.
Spare parts are the third decision, and the cheapest to get right. Straps, closures and small hardware can be held against an order at negligible cost, and having them available turns a returned-module scenario into a two-minute repair. Our production team can hold a reserved material position for those items when it is requested at the time of the main order, which is far cheaper than a later small run.
Takeaway: Tie the generation number to interface geometry, publish a support window for retired modules, and reserve strap and closure spares against the main order, because all three cost little and each prevents a class of complaint.
Interface-defined, accessory-compatible and decorative modularity compared
Setting the three meanings side by side makes the purchasing decision straightforward. The comparison below is deliberately blunt about verifiability, because that is the axis that separates them most cleanly.
| Criterion | Interface-defined | Accessory-compatible | Decorative |
|---|---|---|---|
| Verifiable by a buyer | Yes, by measurement | Partly, by trial | No |
| Reorder in two years | Fits, if contract held | Usually fits, may not | Nothing to reorder |
| Third-party modules | Possible | No | No |
| Development cost | Highest | Moderate | Lowest |
| Documentation burden | A controlled drawing | A sample reference | None |
| Typical failure | Contract not maintained | Silent geometry change | Buyer plans a range on it |
| Suits | Multi-season ranges | One or two seasons | Styling only |
The typical-failure row is the one to read twice. Interface-defined modularity fails through neglect rather than through bad engineering: the contract exists and then nobody maintains it. Accessory-compatible modularity fails through a substitution nobody announced. Decorative modularity fails at the planning stage, when a buyer builds a range around a capability that was never there.
Cost should be read alongside suitability rather than in isolation. Interface-defined development costs more in season one and less in every season after, which is why the higher initial figure is usually the lower total by season three. Buyers comparing quotes across suppliers should compare three-season totals rather than first-season unit prices.
Judgement: Choose interface-defined modularity for anything planned past two seasons, accessory-compatible for a short range, and never plan a module roadmap on a decorative panel, however convincing the exterior looks.
What modularity costs, stated honestly
Modularity is not free, and a specification that pretends otherwise will be caught out in the field. Four costs are real. Weight: an attachment face, its backing and its anchoring add mass that is carried every day whether or not a module is fitted. Unit cost: the face and its construction add labour and material at every unit. Complexity: every module becomes a separate reference with its own forecast, its own minimum and its own obsolescence risk, so a roster of six multiplies the planning work by six. User education: a system has to be explained, and an unexplained system is used as a plain bag.
The weight penalty deserves a number rather than an adjective. Weigh a first-off carrier against a non-modular bag of the same litre capacity, put the difference in the range brief, and let the channel decide whether the trade is acceptable; several programmes have dropped modularity on exactly that measurement and been right to do so. Programmes building a carry-on travel platform with strict weight limits have abandoned modularity on exactly this measurement, and correctly so.
The education cost is the one most often ignored and most cheaply addressed. A single card explaining how to weave a strap, where modules belong and what the closure should look like when seated removes a large share of returns. It costs a fraction of a per-unit discount and protects the review score of the whole range.
None of these costs argue against modularity; they argue against unexamined modularity. A programme that has measured the weight penalty, costed the SKU load and written the instruction card has done the work, and can expect the benefits - longer range life, accessory margin, repairability - to arrive as planned.
Spec rule: Measure the empty-weight penalty on a first-off carrier, cost the module SKU load across the forecast horizon, and ship an instruction card with every modular reference, because all three costs are predictable and all three are cheaper to address before launch.
Writing a modularity claim a buyer can verify
A verifiable claim names the interface, the tolerance and the evidence. It reads like a specification rather than like marketing: webbing width, row spacing, anchoring repeat, backing stack, engaged-row minimum, mass band per module class and the test methods behind each. Every element can be checked on a sample, which is what makes the claim worth the paper it is printed on.
Evidence is the second half. Three methods carry most of the load: seam and tensile behaviour of the attachment face measured to ASTM D5034, abrasion life of the webbing face where re-attachment is frequent, checked to ISO 12947, and cartonised transit simulation under ISTA 3A for structured carriers. Shipment release is assessed against ISO 2859-1, general level II, with the acceptance quality limit set at 2.5 and zero tolerance for any critical defect.
The SGS-verified production base behind this work covers 4,950 m², running 7 production lines and 149 machines with 137 people, and 200,000 units per month of capacity. The founder has been in bag production since 2004 and the business dates from 2014. Sampling opens the programme, a pre-production sample follows, release inspection at AQL 2.5 comes next, and shipment closes it, with a document produced at each gate.
Minimum runs start at 500 units and quotations, issued FOB Xiamen, are returned within one to two working days of a complete brief. A first sample takes 6-10 working days, rising to 12-15 working days for unfamiliar constructions, followed by 35-50 days of bulk production. Settlement is T/T 30/70. Sampling is charged at USD 50-150 and credited against the order, while tooling or screens are quoted between USD 300 and USD 2,500. Budget 25-35 days for ocean freight, 5-8 days by air and 3-5 days for express; container planning uses 28 CBM in a 20GP and 68 CBM in a 40HQ.
When modularity is the wrong answer
Four situations argue against it, and a supplier who never says so is not a useful partner. A single unchanging duty: if the bag will do one thing for its whole life, a fixed construction is lighter, cheaper and simpler. A weight-critical channel: measured weight penalties that matter to the buyer should decide the question. A minimal stock-keeping appetite: retailers who will not merchandise multiple references will not make a modular range work. A fashion-led cycle: where the exterior changes every season, a stable interface is an obstacle rather than an asset.
A fifth situation is internal rather than market-facing: an organisation unwilling to maintain a contract. Interface-defined modularity requires someone to own the drawing, review substitutions and issue revisions. Without that person, the programme slides into accessory-compatible behaviour while still claiming the stronger label, which is the worst of the three outcomes.
Programmes in these situations should still borrow one idea from modular thinking: write the specification down. A fixed bag with a proper drawing, a declared material set and a revision history behaves better across reorders than a modular range with none of those things. The discipline transfers even when the architecture does not.
Buyers weighing this decision against a chassis-based carry range should run the three-season total rather than the first-season quote, because that is where the two answers actually diverge. The rest of the argument - weight, complexity, education - can then be settled on measured numbers rather than on enthusiasm.
In short: Decline modularity for a single fixed duty, a weight-critical channel, a minimal SKU appetite or a fashion-led cycle, and in every case still write the specification down, because documented discipline reorders better than undocumented architecture.
Frequently asked questions
What does modular actually mean in bag design?
It means function is split across parts joined by a declared interface, so one part changes without forcing the others to change. Three properties make it real: written geometry, functional decoupling and lifecycle compatibility across reorders.
- Interface written as dimensions
- Chassis holds slow-changing parts
What is the difference between interface-defined and decorative modularity?
Interface-defined modularity can be verified by measurement and survives a reorder; decorative modularity only suggests exchangeability with printed grids or unused loops. Only the first supports a module roadmap over multiple seasons.
- Measure, do not read the listing
- Decorative panels mount nothing
Which interface dimensions make modularity verifiable?
Webbing width, vertical spacing between rows, and the anchoring repeat: 25 mm, 38 mm and 50 mm, each with a stated tolerance and a named measurement datum. Without a datum, two parties can measure correctly and disagree.
- Three numbers plus tolerance
- Name the datum
What belongs in the chassis rather than in a module?
Harness and back panel, shell fabric and colourway, and attachment face geometry. These change slowly and are expensive to redevelop. Capacity, organisation, padding and colour coding belong in the module, where change is cheap.
- Allocate by change frequency
- Never put volume in the chassis
How should generations of a modular range be numbered?
Number generations from the interface: alter the geometry and the generation moves; leave it and the number holds. Mark the generation physically on the carrier so owners can identify what they have.
- Geometry defines the generation
- Mark it on the product
What support should a retired module receive?
Announce how many seasons spares will remain available when a module leaves, and reserve strap and closure stock against the main order. Both cost little and prevent the worst complaints from owners with an established kit.
- State the window
- Reserve spares at order time
How much weight does modularity add to a bag?
The attachment face, its backing and its anchoring add mass carried every day, whether or not a module is fitted. Weigh a first-off unit against a non-modular bag of the same capacity and put the figure in the brief.
- Weigh on first-off
- Decide against the channel
Which tests support a modularity claim?
Tensile and seam strength is measured to ASTM D5034, webbing wear to ISO 12947 where re-attachment is frequent, cartonised transit to ISTA 3A, and release to a 2.5 acceptance quality limit under ISO 2859-1, general level II.
- Four named methods
- Reports labelled to the construction
When is modularity the wrong choice for a range?
For a single unchanging duty, a weight-critical channel, a retailer with minimal stock-keeping appetite, or a fashion-led cycle. In each case a fixed construction is lighter, cheaper and simpler to merchandise.
- Four deciding situations
- Still write the specification down
Does modularity always cost more per unit?
The chassis costs more, but accessory margin and range life usually reverse the comparison by season three. Compare three-season totals rather than first-season unit prices when evaluating a modular programme at MOQ 500.
- Compare three seasons
- Accessories carry margin
How is a module capacity stated correctly?
Quote a working range for each module family together with a weight ceiling, and name the part that limits it. A padded camera insert and a document sleeve give way at different points, so one blanket figure misleads whoever reads it.
- Range per family
- Name the limiting part
What sampling time applies to a modular design programme?
Development sampling occupies 6-10 working days, stretched to 12-15 working days where the construction is new to the line. Bulk then needs 35-50 days, and prices reach the buyer within one to two working days of a full brief.
- 6-10 days known builds
- 12-15 days new builds
What are the commercial terms for a modular range?
Entry volume is 500 units per reference on FOB Xiamen terms with T/T 30/70 settlement. Sampling runs USD 50-150 and is credited back, tooling or screens sit between USD 300 and USD 2,500, and ocean freight needs 25-35 days at roughly 28 CBM per 20GP.
- 500 per reference
- 28 CBM per 20GP
Should a modular bag ship with instructions?
Yes. A card showing how to weave a strap, where modules belong and what a seated closure looks like removes a large share of returns, and costs a fraction of a per-unit discount across a 500-unit run.
- Show the seated closure
- Show placement logic